
Featured Steel Products & Coated Solutions (Part 1)
Explore our core manufacturing portfolio. Mill-direct pricing, certified quality standards, and export packaging for global engineering requirements.





Understanding High-Quality CRGO Steel Procurement & Efficiency Metrics
Why modern power grids require cold rolled grain oriented silicon steel with optimized Goss texture, high permeability, and cost-effective direct-factory sourcing strategies.
What is High-Quality CRGO Silicon Steel?
Cold Rolled Grain Oriented (CRGO) steel is an indispensable soft magnetic material used primarily in the cores of electrical power transformers, distribution transformers, and reactors. Unlike non-grain oriented electrical steel (CRNGO), CRGO undergoes complex thermomechanical processing to align its crystal grains tightly along the rolling direction (known as the Goss (110)[001] texture).
This precise crystallographic alignment delivers exceptionally high magnetic permeability and remarkably low core loss (iron loss) when magnetized parallel to the rolling direction, enabling electrical equipment to operate at peak thermodynamic and electrical efficiency.
Re-defining "Best Price" via Total Cost of Ownership (TCO)
In global power engineering procurement, securing the "best price" for CRGO steel extends far beyond the initial purchase price per metric ton. True economic efficiency must account for no-load transformer losses over a 30-year operational lifecycle.
Choosing high-grade CRGO with lower specific core loss (P1.7/50Hz) drastically reduces no-load loss capitalized costs ($/kW), allowing transformer OEMs to pass stringent energy efficiency standards (such as EU Ecodesign Tier 2, US DOE 2016, and China GB 20052) while minimizing total material cost.
Technical Roadmap & Future Outlook for CRGO Silicon Steel
Advanced metallurgical breakthroughs, domain refinement techniques, and ultra-thin rolling technologies driving the next generation of transformer core materials.
Laser Domain Refinement (LDR)
By applying high-energy laser irradiation or mechanical scratching onto the CRGO strip surface, magnetic domain walls are artificially narrowed. This drastically reduces anomalous eddy current losses, cutting total core loss by 8% to 15% without altering the chemical composition of the steel substrate.
High Magnetic Induction (Hi-B)
Next-generation Hi-B CRGO grades utilize aluminum nitride (AlN) or manganese sulfide (MnS) inhibitors with modified cold-rolling reduction schedules. They achieve a higher magnetic polarization at 800 A/m ($B_{800} \ge 1.90 \text{ Tesla}$), allowing engineers to increase operating flux densities while downsizing core dimensions.
Ultra-Thin Gauges (0.18mm - 0.23mm)
Traditional CRGO laminations relied on 0.27mm to 0.35mm thickness. The modern technical roadmap shifts toward ultra-thin gauges (0.18mm, 0.20mm, and 0.23mm) combined with advanced tension coatings (C-5 class insulation) to combat high-frequency harmonic losses in converter and traction transformers.
Technical Benchmark: CRGO Grade Specifications & Specific Losses
| CRGO Grade Category | Nominal Thickness (mm) | Max Core Loss P1.7/50Hz (W/kg) | Min Magnetic Induction B800 (T) | Primary Application Target |
|---|---|---|---|---|
| Conventional CRGO (M-4 / M-5) | 0.27 - 0.30 | 1.05 - 1.20 | 1.82 - 1.85 | Standard Distribution Transformers (11kV / 33kV) |
| High-B CRGO (23Q100 / 27Q100) | 0.23 - 0.27 | 0.90 - 1.00 | 1.89 - 1.92 | High-Efficiency Power Transformers & Industrial Grids |
| Laser Refined Hi-B (23QG085) | 0.23 | 0.80 - 0.85 | 1.92 - 1.94 | EHV / UHV Grid Step-Up Transformers & Green Energy |
| Ultra-Thin Laser Refined (18QG075) | 0.18 - 0.20 | 0.70 - 0.75 | 1.93 - 1.95 | Ultra-High Efficiency Grid Core & Solar Inverter Units |
Tailored Engineering Solutions for Global Power Infrastructure
Custom core laminations and slit coils engineered to solve specific thermal, acoustic, and magnetic challenges across diverse energy domains.
1. Renewable Energy & HVDC Transmission
Solar PV farms and offshore wind turbines generate complex voltage harmonics. Our laser-refined ultra-thin CRGO steel maintains magnetic stability under high harmonic loads, preventing premature thermal degradation in transformer cores and step-up stations.
2. Low-Noise Urban Distribution Grids
Magnetostriction in CRGO laminations causes audible transformer hum in densely populated residential areas. By controlling grain domain structures, our low-magnetostriction CRGO grades cut noise levels by up to 5 to 8 dB(A), ensuring municipal acoustic compliance.
3. EV Charging Infrastructure & Reactors
High-power fast-charging hubs rely on ultra-compact DC fast-charging transformers and smoothing reactors. High permeability Hi-B CRGO coils allow maximum energy density, smaller footprint, and minimized heat dissipation under rapid load variations.
China Factory 4.0: Supply Chain Resilience & Cost Advantage
How our integrated production infrastructure, automated quality controls, and direct mill-to-client logistics eliminate market volatility for international buyers.
Full-Process Metallurgical Quality Control
Our production facilities utilize state-of-the-art continuous tandem cold rolling mills, high-temperature box annealing furnaces, and automated tension coating lines. From raw molten steel refining to final coil slitting, every meter of steel is continuously monitored for gauge uniformity, surface flatness, and magnetic consistency.
- Automated Laser Thickness Gauging: Maintains tolerance within ±0.005mm.
- Online Single Sheet Iron Loss Testing: 100% verification of core loss standards.
- C-5 Inorganic Coating Application: Superior interlaminar resistance & stacking factor.
Why Direct Factory Sourcing Guarantees "Best Price"
Procuring directly from our Tianjin manufacturing base bypasses multiple tiers of international trading intermediaries, stockists, and agent markups. Buyers secure authentic factory pricing while receiving custom slitting (strip width down to 20mm), cut-to-length lamination processing, and specialized export packaging.
- Scale Economies: 100,000+ metric tons monthly capacity lowers fixed costs.
- Port Proximity Advantage: Strategically situated near Tianjin Port for rapid FOB/CIF shipping.
- Buffer Stock Management: Year-round master coil inventory ensures fast lead times.
Localization Support & International Quality Compliance
Complete alignment with global electro-technical benchmarks, rigorous quality certification, and tailored logistic protection for international tenders.
Standard Compliance
Our CRGO steel coils fully meet and exceed global electro-technical specifications including IEC 60404-8-7, ASTM A876, EN 10107, and JIS C2553. Mill Test Certificates (MTC) according to EN 10204 3.1 / 3.2 are provided with every shipment.
Third-Party Inspection
We routinely facilitate full third-party inspection (TPI) services with international testing agencies such as SGS, Bureau Veritas, TÜV, and Intertek. Inspections cover Epstein frame loss testing, chemical composition, coating thickness, and edge burr verification.
Seaworthy Export Packing
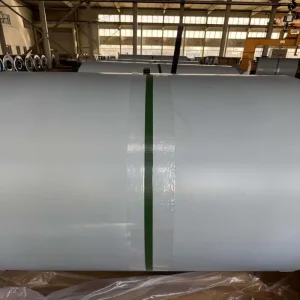
Coils are protected with anti-rust VCI paper, HDPE plastic wrapping, galvanized steel outer sleeves, and sturdy eye-to-sky / eye-to-side hardwood skids secured with high-tensile steel strapping to prevent ocean transit damage.
Global Enterprise Sourcing Checklist for CRGO Silicon Steel
A practical technical checklist for transformer engineers and procurement officers to streamline inquiry specifications and guarantee exact material matching.
When issuing an RFQ (Request for Quotation) for CRGO silicon steel coils or slit strips, providing the following parameter set ensures rapid, accurate mill pricing and technical verification:
1. Magnetic & Physical Grade
Specify the target core loss (e.g., Max 0.85 W/kg at 1.7T/50Hz) or standard grade code (e.g., 23QG085, M-4, NV85-23).
2. Dimensional Tolerances
Specify nominal thickness (0.18mm, 0.20mm, 0.23mm, 0.27mm, 0.30mm) and required strip width tolerance (e.g., +0/-0.2mm).
3. Insulation Coating Class
Request C-5 inorganic tension coating for oil-immersed transformers, or high-temperature coating for dry-type units.
4. Packaging & Coil Parameters
Specify maximum coil weight (e.g., 2.0 to 5.0 MT), coil inner diameter (508mm / 610mm), and skid orientation (Eye to Sky or Eye to Side).
Featured Steel Products & Coated Solutions (Part 2)
Complementary steel supply capabilities including galvanized coils, greenhouse structural tubes, alloy coatings, and structural plates.






Frequently Asked Questions: High-Quality CRGO Steel Sourcing
Direct, expert answers addressing technical, commercial, and logistics inquiries for global electrical steel buyers.
Get Mill-Direct CRGO Pricing & Technical Support
Connect with our senior metallurgical engineers and export pricing specialists today. Receive custom technical proposals, core loss calculations, and mill-direct quotations within 24 hours.