
Featured Steel Products & Tubular Solutions
Explore our certified mill-direct steel portfolio, including high-strength HRPO hollow sections, spiral pipes, cold-rolled sheets, and specialized metallic coated steel coils engineered for demanding structural applications.


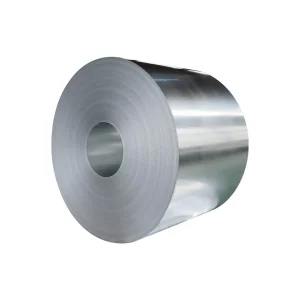


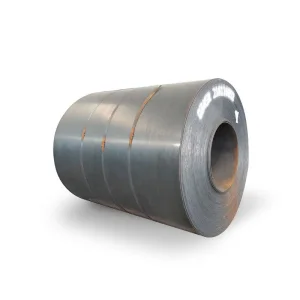

Metallurgical Foundations & Surface Processing Engineering of HRPO Steel Tubing
In modern structural engineering and precision mechanical fabrication, Hot Rolled Pickled and Oiled (HRPO) steel tubing represents a critical technological bridge between unpickled hot-rolled carbon steel and high-cost cold-rolled tubing. Unprocessed hot-rolled steel coil naturally develops a dark, abrasive iron oxide scale (primarily consisting of $Fe_3O_4$, $Fe_2O_3$, and $FeO$) during cooling at temperatures above 575°C. When this scale is left intact, it induces severe tool wear during roll forming, impairs high-frequency electric resistance welding (HFW/ERW) consistency, and prevents direct surface painting, powder coating, or plating without costly mechanical grit-blasting.
As a premier Hot Rolled Pickled And Oiled Steel Tubing Supplier, our production process subjects high-grade hot-rolled coils to an automated, continuous hydrochloric acid (HCl) pickling bath. This chemical bath completely dissolves the mill scale, exposing a clean, uniform, silver-white metallic substrate. Immediately following chemical descaling and neutral electro-hydraulic rinsing, electrostatic oil applicators deposit a micro-thin layer of synthetic rust-preventative oil (typically $1.0 - 2.5 \text{ g/m}^2$). This coating guarantees extended oxidation resistance during transoceanic transit and multi-month warehouse storage while maintaining total compatibility with downstream stamping lubricants and automated degreasing systems.
Comparative Metallurgy: HRPO vs. Cold Rolled (CR) vs. Bare Hot Rolled (HR)
To assist procurement directors and chief mechanical design engineers in optimizing material cost-to-performance ratios, the technical matrix below outlines key physical, mechanical, and surface properties across standard flat-rolled steel tube feedstock grades:
| Performance Parameter | Bare Hot Rolled (HR) Tubing | HRPO Steel Tubing (Our Spec) | Cold Rolled (CR) Tubing |
|---|---|---|---|
| Surface Condition | Dark mill scale ($Fe_3O_4$), rough, prone to flaking | Scale-free, smooth silver-gray with protective oil film | Bright, mirror-smooth, oil-coated or dry |
| Surface Roughness ($R_a$) | $R_a \ge 3.2 - 6.3 \, \mu\text{m}$ | $R_a \le 1.2 - 1.6 \, \mu\text{m}$ | $R_a \le 0.4 - 0.8 \, \mu\text{m}$ |
| Tooling & Die Wear Impact | High tool abrasion due to hard oxide scale | Minimal tooling wear; smooth tube forming | Extremely low tooling wear |
| Weld Seam Integrity (ERW) | Scale inclusions can cause seam porosity | Clean fusion zone; high-frequency weld perfection | Optimal fusion zone perfection |
| Direct Paint / Powder Adhesion | Requires pre-blasting or intensive washing | Excellent after standard alkaline degreasing | Superior direct paint adhesion |
| Gauge Thickness Range | $1.5\,\text{mm} - 12.0\,\text{mm}+$ | $1.2\,\text{mm} - 8.0\,\text{mm}$ | $0.4\,\text{mm} - 3.0\,\text{mm}$ |
| Cost Efficiency Index | Baseline Economy ($100\%$) | Optimal Value ($112\% - 118\%$) | Premium Cost ($140\% - 160\%$) |
China Industry 4.0: Supply Chain Resilience & Manufacturing Efficiency
Our state-of-the-art manufacturing complex in Tianjin leverages cutting-edge China Industry 4.0 smart factory integration. By unifying continuous coil slitting, automated HF induction welding mills, inline ID/OD weld flash removal, and full-spectrum automated Non-Destructive Testing (NDT) within a single Manufacturing Execution System (MES), we deliver unprecedented dimensional consistency and batch-to-batch repeatability.
Inline multi-axis laser sensors verify tube outer diameter (OD), wall thickness symmetry, and corner radii for SHS/RHS square and rectangular profiles every 0.5 seconds, eliminating dimensional drift.
Equipped with automated carbide tungsten cutters, our mills shave the internal weld flash down to $\le 0.1\,\text{mm}$ (or completely flush for mandrel-drawn tubes), preventing interference during hydraulic rod insertion or sleeve coupling.
Every linear meter of weld seam undergoes continuous inline Eddy Current and Ultrasonic NDT inspection certified to ASTM A513 and EN 10305-3 specs, automatically marking and ejecting sub-standard segments.
Macro Industry Solutions & Precision Sector Applications
Due to its superior combination of high structural yield strength, clean surface aesthetic, and excellent drawability, HRPO steel tubing serves as a core engineering material across critical global industrial sectors:
Automotive Chassis & Structural Components
Widely specified for automotive control arms, suspension link subframes, seat frames, driveshafts, and instrument panel supports. Scale-free HRPO steel eliminates tool fouling in high-speed robotic stamping lines and ensures defect-free robotic MIG/MAG welding.
Heavy Machinery & Agricultural Attachments
Extensively utilized for excavator boom supports, forklift mast structures, agricultural harvester frames, and hydraulic cylinder casing sleeves. The high yield strength grades (S355JR / ASTM A513 Type 1) support maximum dynamic fatigue resistance.
Precision Fitness, Furniture & Architectural Systems
Preferred by premium commercial fitness equipment manufacturers and architectural steel designers. HRPO square and round tubes accept high-grade polyester powder coating directly after basic solvent degreasing, yielding a flawless high-gloss finish.
Solar Tracker Torque Tubes & Energy Structures
Engineered to withstand torsional shear forces in utility-scale solar tracking mounting structures. Precision HRPO torque tubes are post-galvanized or painted with specialized outdoor coatings to survive 25+ years in harsh desert or coastal environments.
Global Procurement Requirements & Strict Technical Compliance
Navigating international steel supply chains demands absolute adherence to global standards, comprehensive quality certification, and robust seaworthy packaging protocols. As an audited global supplier, Step Million Steel Supply Chain Co., Ltd. ensures full traceability and strict compliance with global technical benchmarks:
| Standard Specification | Material / Steel Grades | Dimensional & Tolerance Scope | Key Mechanical Testing Requirements |
|---|---|---|---|
| ASTM A513 Type 1A (HRPO) | 1008, 1010, 1015, 1020, 1026 | OD: 12.7mm - 168.3mm WT: 1.2mm - 8.0mm |
Flare test, Flattening test, Tensile & Yield, Ultrasonic Seam Check |
| EN 10305-3 / EN 10305-5 | E195, E235, E275, E355+AR/+N | Round, SHS & RHS Profiles Precision WT: $\pm 0.08\,\text{mm}$ |
Drift expanding test, Flattening, Surface Roughness Measurement ($R_a$) |
| JIS G3445 / JIS G3131 | STKM 11A, STKM 12A/C, SPHC, SPHD | JIS Standard Precision Mechanical Tubes | Chemical ladle analysis, Bending radius validation, Tensile elongation |
| GB/T 13793 / GB/T 6728 | Q195, Q235B, Q355B/C/D | Structural Hollow Sections & Mechanical Pipes | Charpy V-notch impact testing (at $-20^\circ\text{C}$ for Q355D), Hydrostatic test |
Seaworthy Protection & Anti-Rust Packaging Standard
To prevent atmospheric corrosion during humid sea transit, our finished HRPO tubes receive a multi-layer protective wrap consisting of:
- Synthetic Electrostatic Oil Layer: Uniform micro-film coating providing up to 6 months of rust prevention under sheltered storage.
- VCI (Volatile Corrosion Inhibitor) Paper: Sealed inner lining that emits protective vapor molecules to inhibit active oxidation.
- HDPE Woven Plastic Sheathing: High-density waterproof outer wrapping bound with heavy-duty steel strapping.
- Beveled Edge Protectors & Wooden Cradles: Rubber or plastic end caps for threaded/beveled tube ends and custom wooden saddles for container/breakbulk shipping.
Technology Roadmap & Future Outlook (2025 – 2030)
As the global steel manufacturing industry accelerates toward decarbonization and advanced lightweighting, our technology engineering division is actively pursuing next-generation innovations across HRPO tube processing:
Closed-Loop Eco-Pickling & Acid Recovery
Implementing 100% closed-loop Hydrochloric Acid regeneration plants that recover free acid and convert iron chloride byproducts into pure iron oxide powder for ferrite magnet industries, reducing effluent emissions to zero.
Ultra-High Strength HRPO Alloys (AHSS)
Developing pickled and oiled tubes utilizing Advanced High-Strength Steels (AHSS) with yield strengths surpassing 700 MPa (such as S700MC), enabling automotive OEMs to reduce structural component wall thickness by up to 25% without sacrificing crash safety.
AI-Driven Adaptive Welding Thermal Control
Incorporating neural-network infrared thermal imaging at the high-frequency weld squeeze rolls to dynamically adjust induction power in real time, guaranteeing 100% grain refinement across variable line speeds.
Localized Technical Support, Prototyping & On-Site Compliance
Understanding that global procurement involves complex local engineering approval processes, Step Million Steel provides tailored technical support for engineering firms and Tier-1 automotive sub-contractors worldwide:
Custom Tooling & Roll-Die Development
Our in-house die workshop features over 20 senior R&D tooling engineers capable of designing and machining custom forming dies for non-standard oval, D-shape, or heavy-wall rectangular HRPO profiles within 14 days of CAD drawing approval.
Third-Party Inspection & Mill Test Certification
Every shipment is accompanied by a mill test certificate (MTC) conforming to EN 10204 3.1 or 3.2. We fully facilitate on-site inspection, sampling, and mechanical testing by independent agencies including SGS, TÜV, Bureau Veritas (BV), and Intertek.
Complete Steel Pipe, Coil & Sheet Product Catalog
Browse our secondary catalog of premium steel products manufactured to rigorous global specifications and available for worldwide delivery.




Frequently Asked Questions: Technical Engineering & Global Sourcing
Get quick, authoritative answers to the most common metallurgical, manufacturing, and commercial questions regarding Hot Rolled Pickled and Oiled Steel Tubing.
What is the primary technical advantage of choosing HRPO steel tubing over standard Hot Rolled black steel tubing?
HRPO tubing completely eliminates abrasive iron oxide mill scale via hydrochloric acid pickling. This provides a clean, smooth surface ($R_a \le 1.6\,\mu\text{m}$), extends stamping and cutting die life by up to 300%, allows direct powder coating or painting without grit-blasting, and ensures clean, defect-free welds during high-frequency ERW mill forming or downstream customer fabrication.
How long does the rust-preventative oil on HRPO steel tubing last during transit and storage?
Our electrostatic applicators deposit a specialized synthetic rust-preventative oil ($1.0 - 2.5\,\text{g/m}^2$) that offers effective oxidation protection for 3 to 6 months under standard indoor dry warehouse conditions. When combined with our multi-layer VCI paper and waterproof plastic packaging, the tubing safely withstands tropical maritime export shipping.
Can HRPO steel tubing be powder coated directly without pre-treatment?
While HRPO steel has no hard oxide scale to blast off, the protective oil film must be removed prior to painting or powder coating. A standard mild alkaline wash or multi-stage degreasing line easily cleans the surface, allowing exceptional paint adhesion and smooth cosmetic appearance without mechanical abrasion.
What dimensional tolerances can your mill achieve on HRPO square and rectangular hollow sections?
Equipped with real-time laser profiling sensors and high-precision sizing stands, our mills hold outer dimensional tolerances within $\pm 0.2\%$, wall thickness within $\pm 0.05\,\text{mm}$, and corner squareness within $90^\circ \pm 0.5^\circ$, fully meeting or exceeding EN 10305-5 and ASTM A513 standards.
Do you offer internal weld seam flash control (ID bead scraping) for telescope or mandrel applications?
Yes. Our automated tube mills feature internal weld bead trimming capabilities that reduce the internal flash height to $\le 0.1\,\text{mm}$ (or completely flush), essential for telescoping structures, drive shafts, and hydraulic sleeve fittings.
What is the typical lead time and minimum order quantity (MOQ) for custom HRPO tube sizes?
For standard OD and wall thicknesses, our MOQ is 5 to 10 metric tons per size with a production lead time of 15 to 20 days. For custom profiles requiring specialized roll-die machining, die development takes approximately 10 to 14 days, with initial sample validation delivered shortly after.
Which mill certificates and quality documentations accompany the shipment?
Every shipment includes an original EN 10204 3.1 Mill Test Certificate detailing chemical heat analysis, mechanical tensile/yield tests, flattening/flare verification, and ultrasonic NDT test results. EN 10204 3.2 certificates issued by third-party inspectors (SGS/TÜV) are available upon request.
How does HRPO steel tubing compare economically with Cold Rolled (CR) tubing?
HRPO steel tubing typically costs 25% to 40% less than Cold Rolled steel tubing while offering virtually identical surface cleanliness, excellent drawability, and comparable weld quality in gauge thicknesses from $1.5\,\text{mm}$ to $6.0\,\text{mm}$, making it the most cost-effective solution for heavy-duty structural applications.