
Featured Steel Coil & Tubing Solutions
Explore our premium factory-direct portfolio manufactured under strict ISO 9001 and IATF 16949 quality management systems.




Engineering Hot Rolled Oiled Steel Coils: An Executive Technical Brief
Understanding the microstructural mechanics, chemical pickling protocols, and oil-film passivation behind world-class hot rolled oiled steel coil manufacturing.
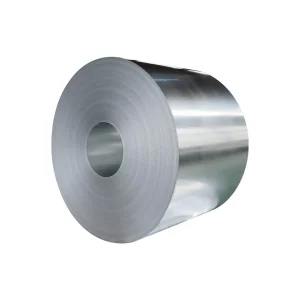
In modern industrial metallurgy, **Hot Rolled Oiled (HRO) Steel Coils**—frequently supplied as Pickled and Oiled (HRPO)—represent a critical intermediary material bridging raw structural hot-rolling and high-precision downstream fabrication. When molten steel slabs undergo thermo-mechanical controlled processing (TMCP) at temperatures exceeding 1,100°C (2,012°F), a complex oxide crust known as mill scale (composed of layers of hematite Fe₂O₃, magnetite Fe₃O₄, and wüstite FeO) forms on the strip surface. For critical engineering applications requiring smooth deep-drawing, precision roll forming, laser cutting, or direct welding without abrasive surface pre-treatment, unpickled hot-rolled steel presents severe operational challenges.
As a leading **Hot Rolled Oiled Steel Coil Manufacturer & Factory**, our facility utilizes state-of-the-art continuous hydrochloric acid (HCl) pickling lines integrated with high-efficiency electrostatic oiling technology. Through controlled chemical dissolution, the abrasive mill scale is completely stripped, revealing a pristine, silver-grey matte metallic substrate. Immediately post-pickling and rinsing, an engineered hydrocarbon or synthetic rust-preventative oil film is uniformly applied. This oil coating serves a dual purpose: it acts as a robust barrier against atmospheric oxidation (rusting) during ocean transit and long-term storage, while simultaneously functioning as a boundary lubricant during initial stamping, punching, and roll-forming operations.
Comprehensive Technical Specifications & Metallurgical Matrix
Engineering consistency driven by strict adherence to international standards including ASTM, EN, JIS, and GB/T.
| Steel Grade Category | Standard Equivalents | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) | Primary Industrial Use |
|---|---|---|---|---|---|
| Commercial & Deep Drawing | ASTM A1011 CS Type B / SPHC / SPHD / DD11 | 170 - 300 | 270 - 440 | ≥ 30 - 38 | Stamping, automotive interior brackets, HVAC ducts, general hardware |
| Structural Carbon Steel | ASTM A36 / S235JR / SS400 / Q235B | ≥ 235 | 360 - 510 | ≥ 26 | Construction frames, welded pipes, racking systems, highway guardrails |
| High-Strength Low-Alloy (HSLA) | ASTM A1011 HSLAS Gr 50 / S355DD / Q355B | ≥ 355 | 470 - 630 | ≥ 20 | Heavy machinery chassis, crane booms, trailer side-rails, agricultural implements |
| Automotive Structural Steel | EN 10149-2 S500MC / S700MC | 500 - 700 | 550 - 860 | ≥ 12 - 14 | Chassis side members, safety reinforcement beams, crash structures |
| Gas Cylinder & Pressure Vessel | GB/T 6653 HP295 / EN 10120 P265NB | ≥ 295 | 440 - 570 | ≥ 22 | LPG cylinders, compressed air tanks, welded pressure tubing |
Electrostatic Oiling Density
We deploy high-voltage electrostatic oil applicators that atomize rust-preventative oil droplets, depositing a highly uniform film ranging from 0.5 g/m² (light oil for immediate stamping) up to 2.5 g/m² (heavy oil for long-distance maritime export). This eliminates dry spots and excess pooling.
Tension Leveling & Flatness
To prevent edge wave, center buckle, and crown distortion during high-speed laser cutting, our coils pass through continuous stretch-tension levelers. Thickness tolerance is governed tightly within ±0.03 mm to ±0.08 mm depending on total strip gauge.
Eco-Friendly Rust Inhibitors
Our formulation utilizes barium-free, non-toxic, easily degreasable rust-preventative oils. Coils can be processed downstream without requiring specialized solvent baths—standard alkaline washing stations completely clear the surface prior to painting or galvanizing.
Global Commercial & Industrial Landscape of Hot Rolled Oiled Steel
Analysis of regional consumption patterns, international trade corridors, and supply chain dynamics driving global demand.
The global trade in Hot Rolled Oiled Steel Coils is experiencing structural shifts driven by nearshoring, infrastructure modernization, and stringent environmental mandates. Historically categorized as a secondary raw material, HRPO steel has rapidly elevated its status to a primary feedstock across major manufacturing hubs in North America, Europe, Southeast Asia, and the Middle East.
In **North America**, the automotive and heavy transport sectors have accelerated their adoption of high-strength HRPO coils (such as ASTM A1011 HSLAS Grade 50 and 80) to replace heavier cold-rolled components. Because HRPO provides surface cleanliness comparable to cold-rolled steel at a significantly lower energy and monetary cost per ton, OEM stampers utilize it for frame rails, cross-members, and suspension arms. Furthermore, stringent EPA air-quality regulations have pushed fabricators away from in-house chemical pickling, driving direct sourcing of pre-pickled and oiled coils from advanced offshore mills.
In the **European Union**, the dynamic is governed by the Carbon Border Adjustment Mechanism (CBAM) and the transition toward "Green Steel." European manufacturers increasingly require mill test certificates detailing Scope 1, 2, and 3 carbon emissions. Our production routes integrate energy-efficient regenerative combustion burners in reheating furnaces and closed-loop acid recovery systems, ensuring full compliance with European sustainability benchmarks while delivering superior metallurgical properties.
In **Developing Global Markets** (Latin America, Middle East, and SEA), massive investments in solar photovoltaic infrastructure, urban transit, and agricultural automation have triggered unprecedented demand for structural hot-rolled oiled steel. The material’s resistance to flash rusting during tropical transit makes it the ideal choice for regional service centers that perform slitting, blanking, and customized profile manufacturing.
Future Industry Trends & Metallurgical Innovations
How cutting-edge steelmaking technologies are reshaping surface aesthetics, mechanical strength, and decarbonization.
Hydrogen-Based DRI & EAF Steelmaking
Transitioning from traditional Blast Furnace-Basic Oxygen Furnace (BF-BOF) routes to Direct Reduced Iron (DRI) powered by green hydrogen and Electric Arc Furnaces (EAF). This cuts embedded carbon footprint by up to 60% without compromising coil formability.
AI-Driven Surface Defect Inspection
Real-time machine vision systems using high-speed optical cameras and neural networks inspect 100% of the coil surface at line speeds up to 300 m/min. Pinholes, oil streaks, residual scale, and mechanical scratches are flagged and mapped automatically.
Dry-Lube & Wash-Free Oils
Emerging dry-film lubricants applied electrostatically eliminate the traditional liquid oil mess in stamping plants. These polymers double as corrosion barriers during shipping and draw lubricants during pressing, washing off in low-temperature alkaline water.
Micro-Alloying Chemistry Optimization
Precise additions of Niobium (Nb), Vanadium (V), and Titanium (Ti) fine-tune grain boundaries during hot rolling. This achieves ultra-high yield strengths (up to 700 MPa) while maintaining superior bendability and weldability for structural applications.
Localized Application Scenarios & Engineering Case Studies
Targeted material selection guides across key global industrial sectors.
Automotive Chassis & Stamping
Requirement: High fatigue strength, flawless surface for e-coating, tight thickness tolerances.
Grade Choice: SPHC / SPHD / S355MC.
Application: Control arms, bumper beams, seat frame structures, wheel rims. Our pickled and oiled surface ensures 100% adhesion for cathodic dip painting (KTL) without scale popping.
Precision Welded Tube Manufacturing
Requirement: Uniform edge slitting, clean weld seam creation, zero mill scale contamination.
Grade Choice: Q235B / Q355B / ASTM A500 Gr B.
Application: ERW high-frequency welded square, rectangular, and round tubes for furniture, scaffolding, and structural columns. Pickled edges extend slitting blade life by 300%.
Solar Racking & Mounting Frames
Requirement: High yield strength, suitability for continuous roll-forming and field punching.
Grade Choice: S355JR / ASTM A1011 HSLAS Gr 50.
Application: Photovoltaic C/U channels, torque tubes, and ground-mount brackets destined for post-galvanizing or direct zinc-aluminum-magnesium coating.
Heavy Machinery & Construction Equipment
Requirement: Deep drawability, heavy-gauge plate precision laser cutting.
Grade Choice: S500MC / S700MC / Q460.
Application: Excavator arms, crane booms, dump truck bodies, and tractor frames where weight reduction and high yield performance are paramount.
HVAC & Electrical Enclosures
Requirement: Smooth surface finish, resistance to storage oxidation, easy bendability.
Grade Choice: DD11 / SPHC.
Application: Commercial air-conditioner compressor housings, electrical transformer boxes, industrial duct flanges, and cable trays.
Agricultural Implements & Storage
Requirement: Abrasion resistance, toughness, cost-effective structural performance.
Grade Choice: ASTM A36 / Q235B.
Application: Grain silo stiffeners, plow blades, harrow frames, and conveyor brackets operating under demanding field conditions.
Macro Supply Chain Solutions & Factory Value-Added Capabilities
End-to-end processing, tailored packaging, and global logistics engineering designed for seamless procurement.
Precision Slitting & Edge Trimming
Equipped with high-precision CNC slitting lines capable of processing coils up to 25mm in thickness down to narrow strip widths of 30mm. Edge conditioning options include mill edge, sheared edge, and rounded edge to prevent cracking during severe bending.
Cut-to-Length & Sheet Leveling
Our heavy-duty hydraulic cut-to-length lines transform master coils into flat sheet plates with zero internal residual stress. Advanced multi-roll levelers compensate for coil set, cross bow, and camber, supplying ready-to-use blanks for laser cutting fabricators.
Seaworthy VCI Export Packaging
To withstand long sea voyages across varying temperature zones, every coil is wrapped in Volatile Corrosion Inhibitor (VCI) anti-rust paper, sealed in heavy-duty galvanized steel outer jackets, fitted with steel edge protectors, and secured on wooden or steel pallets.
Technological Roadmap & Future Outlook (2025 - 2035)
Pioneering the next generation of smart, sustainable, and high-performance flat steel manufacturing.
Zero-Waste Hydrochloric Acid Recovery & Closed-Loop Pickling
Implementation of 99.8% acid recovery systems that convert spent pickling liquor into high-purity iron oxide powder for ferrite magnet manufacturing, completely eliminating liquid effluent waste.
Ultra-Thin Hot-Rolled Strip Production (ESP/FTSR)
Commercialization of Endless Strip Production (ESP) technology to cast and roll hot-rolled oiled steel down to gauges of 0.8 mm, offering direct replacement for cold-rolled steel at 25% lower carbon intensity.
100% Green Hydrogen Metallurgical Reduction
Full integration of green hydrogen direct reduction technology in slab production, achieving near-zero carbon emission status for hot rolled pickled and oiled steel coils supplied globally.
Complete Steel Pipe & Flat-Rolled Product Series
Review our extended product catalogue tailored for global distributors, stockists, and EPC contractors.





Frequently Asked Questions (Technical & Procurement Q&A)
Expert answers addressing engineering specifications, quality assurance, storage life, and international logistics.
What is the primary technical difference between Hot Rolled Black Steel and Hot Rolled Pickled & Oiled (HRPO) Steel?
Hot Rolled Black steel retains its dark, abrasive iron oxide mill scale formed during hot rolling above 1,100°C. In contrast, Hot Rolled Pickled & Oiled (HRPO) steel undergoes continuous hydrochloric acid pickling to strip away all oxide scale, followed by the electro-deposition of a rust-preventative oil film. HRPO offers a smooth, clean matte finish, improved thickness consistency, superior tool life during stamping, and direct paintability/weldability without prior grit-blasting.
How long does the rust-preventative oil coating protect the steel coil against atmospheric corrosion?
Under standard ambient indoor storage conditions (temperatures between 15°C to 25°C and relative humidity below 60%), our standard electrostatic oil application (1.0 to 1.5 g/m²) provides effective corrosion protection for up to 6 months. For transoceanic export, combined with our VCI barrier wrap and desiccants, protection is extended to 12 months. Customized heavy oiling (up to 2.5 g/m²) is available for extreme tropical environments.
Can Hot Rolled Oiled Steel Coils be painted or powder-coated directly upon uncoiling?
No, the protective oil film must be removed prior to painting, powder coating, or hot-dip galvanizing to ensure proper coating adhesion. However, because our oil formulation is water-soluble and synthetic/paraffinic based, it can be easily removed in standard automated industrial degreasing washers using mild alkaline baths at 50°C - 60°C, leaving zero oily residue.
What coil dimensions, inner diameters (ID), and weight ranges can your mill produce?
We manufacture Hot Rolled Oiled Coils in thickness ranges from 1.2 mm to 25.0 mm and strip widths from 600 mm up to 2,000 mm. Standard coil Inner Diameter (ID) options are 508 mm (20 inches) and 610 mm (24 inches). Individual coil weights range from 5 metric tons up to 30 metric tons, tailored to match the uncoiler capacity of your production facility.
Which international quality certifications and testing documentation accompany each shipment?
Every coil order is issued a comprehensive Mill Test Certificate (MTC) conforming to EN 10204 3.1 or 3.2. Detailed test data includes heat chemistry (C, Mn, Si, P, S, Cr, Ni, Nb, V, Ti, CEV), yield and tensile mechanical properties, percentage elongation, bending tests, coating weight (g/m²), and ultrasonic flaw inspection reports. Our factory is fully certified under ISO 9001, ISO 14001, ISO 45001, and IATF 16949.
How does HRPO steel assist in extending press tooling and die lifespan during deep drawing?
Mill scale on unpickled hot-rolled steel consists of hard iron oxides that act as an abrasive grit during stamping, rapidly eroding expensive carbide dies and causing surface galling. By removing this scale through pickling and applying a uniform oil film, die wear is reduced by up to 70%, tool changeover downtime is minimized, and deep-drawn parts achieve smooth, blemish-free sidewalls.