
Featured Heavy-Duty Steel Pipes & Materials for Finnish Projects
Premium certified tubulars and flat steel products manufactured strictly to EN 10219, EN 10217, and API 5L engineering standards for harsh Nordic climates.


Wholesale High-Quality Hot Rolled Pickled and Oiled Steel Coils for Pipe Fabrication
View Technical Details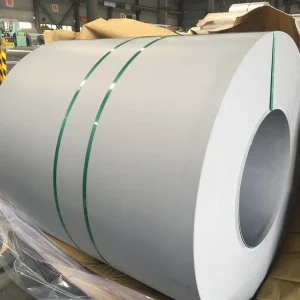
Global Macro Industrial Landscape of Spiral Welded Steel Pipe (SSAW / HSAW)
Spiral Submerged Arc Welded (SSAW) steel pipes—also known as Helical Submerged Arc Welded (HSAW) pipes—represent a cornerstone of modern global civil engineering, deepwater foundation works, and cross-border energy transmission lines. Unlike Longitudinal Submerged Arc Welded (LSAW) or Electric Resistance Welded (ERW) pipes, SSAW pipes are formed by continuously rolling high-grade hot-rolled carbon steel strip coils (HRPO) at a precise helical angle. This spiral geometry permits the manufacture of large-diameter pipes (up to DN3200 / 126 inches) from narrower steel strip feedstocks, offering exceptional structural versatility and economy.
On a global scale, the demand for SSAW steel pipe is driven by rapid urban infrastructure renewal, port expansions, offshore wind turbine foundation installations, and bulk fluid conveyance (district heating, water, and hydrocarbon transport). Modern automated double-sided submerged arc welding (DSAW) technologies ensure that seam welds achieve 100% penetration and mechanical properties matching or exceeding the parent metal, conforming strictly to global benchmarks like API 5L, EN 10219-1, EN 10217-5, and ISO 3183.
Mechanics of Helical Stress Distribution
In spiral welded pipes, the internal pressure induces hoop stress that acts at an angle relative to the helical weld line. Consequently, the principal stress perpendicular to the weld seam is reduced by 30% to 50% compared to a longitudinal seam pipe of equal wall thickness, providing elevated burst-pressure safety margins.
Metallurgical Evolution & Micro-Alloying
Utilizing thermo-mechanically controlled processed (TMCP) coils with micro-alloying elements such as Niobium (Nb), Vanadium (V), and Titanium (Ti), SSAW pipes achieve high yield strengths (e.g., S355J2H up to S460NH, API X70/X80) alongside outstanding low-temperature impact toughness.
Finland's Local Industrial Reality, Climate Challenges & Infrastructure Demand
Finland presents a unique operational landscape for steel pipe manufacturers and structural engineers. Situated in northern Northern Europe with extensive coastal regions along the Gulf of Finland and Bothnian Sea, Finnish infrastructure is subject to sub-arctic climatic extremes, frozen soil dynamics, heavy frost heave, and aggressive marine salinity. Procurement decisions in Finnish hubs like Helsinki, Espoo, Tampere, Turku, Oulu, and Raahe prioritize structural durability, environmental compliance, and long service lifespan.
Key Finnish Sector Demand Drivers:
- Deepwater Marine Piling & Harbor Infrastructure: Expansion of major Finnish ports (Port of Helsinki / Vuosaari, HaminaKotka, Port of Oulu) demands large-diameter SSAW steel bearing piles (conforming to EN 10219-1/2, Grade S355J2H / S355MH) capable of sustaining heavy axial loads, lateral wave action, and winter ice loading.
- Municipal District Heating Trunk Networks (Kaukolämpö): Over 50% of heating in Finland is supplied via centralized district heating. High-pressure steam and hot water main pipelines require heavy-wall spiral welded steel pipes certified to EN 10217-5 (welded steel tubes for pressure purposes under elevated temperatures) with factory-applied 3LPE/3LPP or polyurethane insulation jacket protection.
- Mining, Water Management & Slurry Transport: Northern Finland’s mining clusters (such as Sodankylä, Kittilä, and Kevitsa) require durable, abrasion-resistant, and high-pressure steel pipelines for mine dewatering, tailings disposal, and process water circulation under freezing ground conditions.
- Green Transition & Geothermal Energy Infrastructure: As Finland accelerates toward carbon neutrality, deep geothermal heat projects and hydrogen-ready pipeline corridors necessitate SSAW pipes with strict chemical purity, fine-grained microstructures, and zero-defect NDT compliance.
| Environmental Factor in Finland | Technical Impact on Pipe Steel | Engineered SSAW Solution / Requirement |
|---|---|---|
| Sub-Zero Temperatures (-40°C) | Brittle fracture risk in standard carbon steel welds. | Charpy V-Notch impact testing at -20°C / -40°C (≥ 27 Joules) to EN 10219 S355J2H / S355K2H. |
| Acidic Peat & Marsh Soil | External electrochemical corrosion on buried lines. | 3-Layer Polyethylene (3LPE) or Fusion Bonded Epoxy (FBE) coating to DIN 30670 / ISO 21809-1. |
| Baltic Sea Ice & Brackish Water | Severe corrosion and mechanical ice abrasion on piles. | Heavy-wall SSAW piling pipe with Coal Tar Epoxy or Glass Flake Epoxy underwater splash-zone coatings. |
| Frost Heave & Ground Movement | High bending moment and tensile deformation stresses. | High yield strength S355MH / S460MH TMCP steel with superior elongation capacity (≥ 20%). |
Comprehensive Technical Manufacturing Solutions & Quality Control
To meet the rigorous standards demanded by Finnish structural design codes (SFS-EN) and the Finnish Transport Infrastructure Agency (Väylävirasto), our manufacturing facility implements state-of-the-art automated SSAW production lines. Every pipe length undergoes an integrated quality assurance framework from coil slitting to final delivery clearance.
1. Advanced Double-Sided SAW Welding Process
Our SSAW lines utilize Lincoln Electric multi-wire automatic submerged arc welding systems. The inner weld is executed first, followed immediately by the external weld seam. Precise automatic seam-tracking sensors dynamically adjust torch alignment to guarantee uniform weld reinforcement, perfect bead contour, and zero undercut flaws.
2. Hydrostatic Pressure Testing
100% of pressure pipes undergo full-length hydrostatic testing up to 100% SMYS (Specified Minimum Yield Strength) according to API 5L and EN 10217 specifications. Computer-controlled holding pressure cycles ensure complete seal integrity before NDT evaluation.
3. Comprehensive Non-Destructive Testing (NDT)
Our Quality Assurance program incorporates real-time industrial inspection technologies:
- Offline Automatic Ultrasonic Testing (UT): Full-body inspection of 100% weld seam length for internal voids, cracks, and inclusions.
- Real-Time Industrial X-Ray Radiography (RT): Fluoroscopic examination of pipe end weld zones and suspect UT indications.
- Magnetic Particle Testing (MT) & Visual Inspection: Precise surface inspection of bevel edges and heat-affected zones (HAZ).
European Standards (EN), CE Marking & Finnish SFS Conformance
Entering the Finnish construction and engineering procurement market requires total transparency regarding European directives and harmonized standards under the Construction Products Regulation (CPR 305/2011/EU). All structural steel pipes supplied to Finland must carry valid CE marking and Factory Production Control (FPC) certification accredited by European Notified Bodies.
EN 10219-1 / EN 10219-2
Cold formed welded structural hollow sections of non-alloy and fine grain steels. Defines tolerances, dimensions, sectional properties, and steel grades (S235JRH, S275J0H, S355J2H, S355K2H, S460NH) critical for load-bearing piles and marine structures in Finland.
EN 10217-1 / EN 10217-5
Welded steel tubes for pressure purposes. Specifies non-alloy and alloy steel pipes with defined elevated/low temperature properties. Mandatory for Finnish municipal water mains, thermal plants, and district heating networks.
ISO 3834-2 / EN 1090-1
Quality requirements for fusion welding of metallic materials. Execution of steel structures (EXC1 through EXC4) ensuring complete traceability from raw heat numbers to final inspector signatures on Mill Test Certificates (MTC EN 10204 3.1 / 3.2).
Väylävirasto / Finnish Transport Infrastructure Guidelines
Special localized requirements regarding weld seam impact toughness, corrosion margins, pile clutch welding, and strict dimensional ovality tolerances for bridge and harbor foundation engineering.
Localized Application Scenarios in Finnish Infrastructure
Scenario A: Baltic Deepwater Port Foundation (Helsinki / HaminaKotka)
Challenge: Constructing heavy-duty quay walls and vessel mooring piers in soft clay seabeds subject to winter ice loads (-30°C air temperature, severe saltwater immersion).
Solution: DN1200 x 16mm SSAW steel pile pipes in Grade S355J2H with CVN impact testing at -20°C. Pipes supplied with factory-welded interlocking clutches (interlocks) and external glass-flake reinforced epoxy coating for upper splash zones.
Scenario B: District Heating Trunk Line (Tampere - Espoo Network Expansion)
Challenge: Conveying hot water at 120°C under 1.6 MPa working pressure across rocky, undulating topography with minimal heat loss and zero ground leakage risk.
Solution: EN 10217-5 P235GH / P265GH SSAW pipes in DN800 with 3-Layer Polyethylene (3LPE) external anti-corrosion coating and pre-insulated polyurethane casing, fully inspected by 100% Radiographic Testing.
Technological Roadmap & Future Outlook for SSAW Pipe Manufacturing
As the European steel industry transitions toward sustainable manufacturing under green deal directives, the future of spiral welded steel pipes is defined by three main pillars:
- Green Steel Strip Feeds (Decarbonized Production): Transitioning from traditional blast-furnace hot-rolled coils to Green Hydrogen-based Direct Reduced Iron (DRI) steel strip feeds, dramatically reducing the embodied carbon footprint (CO2 per ton of steel) for zero-carbon infrastructure in Finland.
- Digital Twin & AI-Driven Laser Seam Tracking: Integration of adaptive laser optical seam tracking and AI-based real-time weld pool monitoring to eliminate human error and achieve flawless weld geometries during high-speed HSAW forming.
- Hydrogen-Ready Pipeline Metallurgy: Engineering ultra-clean steel compositions with low sulfur (≤0.002%) and low hydrogen-induced cracking (HIC) sensitivity, preparing future Finnish energy corridors for pure hydrogen transportation.
Frequently Asked Questions (FAQ) for Finnish Procurement Managers
Detailed technical answers to common queries regarding spiral welded pipe sourcing, EN compliance, logistics, and quality assurance in Finland.
What are the key advantages of Spiral Welded (SSAW) pipes over LSAW pipes for Finnish structural piling?
How do you ensure SSAW steel pipes withstand sub-zero Finnish winter temperatures (-40°C)?
Are your spiral steel pipes fully certified for use in EU and Finnish public works tenders?
What anti-corrosion coating options are recommended for buried district heating or acidic soils in Finland?
What is the typical shipping lead time to major Finnish ports such as Helsinki, Kotka, or Turku?
Can you supply custom pipe ends, beveling, and pile interlocks/clutches welded at the factory?
Complete Range of Certified Tubular & Steel Structural Solutions
Explore our full line of galvanized pipes, structural sections, flanged fittings, and specialty cold/hot-rolled steel products available for immediate export to Finland.

Wholesale High Zinc Hot-Dip Galvanized Steel Pipes for Agricultural & Greenhouse Use
View Technical Details
Wholesale High-Quality Hot Rolled Pickled & Oiled (HRPO) Steel with Smooth Finish
View Technical Details
Wholesale China Q195 Q215 Hot Rolled Steel Angle Iron Beam for Structural Applications
View Technical Details
Wholesale Slip-on Plate Flanges & Welding Carbon/Stainless Steel Blind Flanges
View Technical Details
Wholesale Thick-Wall Pre-Galvanized Steel Pipe for High-Load Structural Frames
View Technical Details
High-Quality Thick-Wall Pre Galvanized Steel Pipe for Heavy Commercial Installations
View Technical Details
High-Quality Cold Rolled High Strength Steel Sheets with Extra Deep Drawing Quality
View Technical Details
High-Quality Prime Hot Rolled Pickling and Oiled Steel Coils Supplier & Factory
View Technical DetailsRequire Custom SSAW Steel Pipe Specifications for Your Finnish Project?
Send your project drawings, wall thickness requirements, and EN standards to our engineering team today for an immediate mill-direct quote.
Send Inquiry Now