
Featured Enterprise Steel Coils & Industrial Inventory
Showing 1 - 8 of Factory Direct Line Items

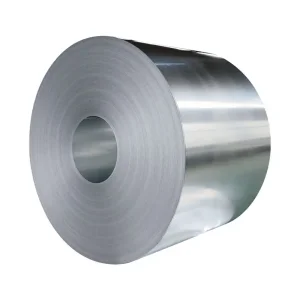
High-Performance Cold-Rolled Non-Grain Oriented Silicon Steel Solutions
An authoritative technical evaluation of CRNGO magnetic laminations, silicon-aluminum alloy composition, core loss dynamics, and global supply chain strategies for electric motor and generator original equipment manufacturers (OEMs).
Isotropic Magnetic Properties
Unlike Grain-Oriented Silicon Steel (CRGO) which exhibits magnetic anisotropy along the rolling direction, Non-Grain Oriented Silicon Steel (CRNGO) provides uniform magnetic permeability in all spatial directions ($360^\circ$). This multi-directional magnetic isotropy is essential for rotating electrical machinery, ensuring minimal eddy current dissipation across rotating magnetic fields.
Low Core Loss & High Permeability
Formulated with controlled additions of silicon ($\text{Si}$) and aluminum ($\text{Al}$), our wholesale silicon steel significantly elevates electrical resistivity while depressing coercivity. This dual thermodynamic enhancement restricts total iron losses—specifically minimizing classical eddy-current loss ($P_e$) and hysteresis loss ($P_h$) during high-frequency alternating magnetization cycles.
Superior Stacking Factor & Interlaminar Isolation
Featuring precision-controlled surface insulation coatings (C-3 organic, C-5 semi-organic chromate-free, and self-bonding varnishes), our CRNGO steel laminations ensure maximum interlaminar resistance. This tight surface tolerance allows motor manufacturers to achieve high stacking factors ($\ge 97\%$), increasing active magnetic volume within motor stators and rotors.
Metallurgical Composition & Crystal Structure Engineering
Cold-Rolled Non-Grain Oriented Electrical Steel is produced through ultra-clean steelmaking (vacuum degassing), continuous slab casting, hot strip rolling, pickling, and specialized cold rolling sequences followed by final decarburization and recrystallization annealing. The secondary annealing stage promotes controlled grain growth (average grain size: 40 μm to 150 μm) while reducing carbon content to below $0.003\%$ to permanently eliminate magnetic aging phenomena.
The incorporation of $1.0\% - 3.5\%$ silicon increases matrix electrical resistivity ($\rho$) from approximately $10\,\mu\Omega\cdot\text{cm}$ in pure iron to over $45\,\mu\Omega\cdot\text{cm}$. Consequently, under alternating magnetic excitation (50Hz / 60Hz / 400Hz+), the induced intra-laminar eddy currents are severely restricted, yielding the thermal efficiency required for Premium Efficiency (IE3), Super-Premium Efficiency (IE4), and Ultra-Premium Efficiency (IE5) electric drives.
Comprehensive CRNGO Grade Matrix & Technical Specifications
Direct comparison of international non-grain oriented silicon steel grades conforming to IEC 60404-8-4, EN 10126, ASTM A677, and JIS C2552 standards.
| Standard Grade (IEC/EN) | Nominal Thickness | Max Core Loss $P_{1.5/50}$ (W/kg) | Max Core Loss $P_{1.5/60}$ (W/kg) | Min Magnetic Flux Density $B_{5000}$ (T) | Typical Applications |
|---|---|---|---|---|---|
| M270-35A | 0.35 mm | 2.70 | 2.10 | 1.60 | High-Frequency Motors, EV Traction Drives |
| M300-35A | 0.35 mm | 3.00 | 2.30 | 1.62 | Hermetic Compressors, High-Speed Rotors |
| M330-50A | 0.50 mm | 3.30 | 2.55 | 1.63 | IE4 Premium Efficiency Motors, Servo Actuators |
| M350-50A | 0.50 mm | 3.50 | 2.70 | 1.64 | Industrial Induction Motors, Wind Generators |
| M470-50A | 0.50 mm | 4.70 | 3.60 | 1.66 | Standard IE2 Motors, Power Tool Armatures |
| M600-50A | 0.50 mm | 6.00 | 4.60 | 1.68 | Home Appliance Motors, Fan Coils |
| M800-65A | 0.65 mm | 8.00 | 6.10 | 1.70 | Small Power Transformers, Ballasts, EI Stamping |
Insulation Coating Classification & Surface Finishes
C-3 / Organic Coating (Clear / Pigmented)
Consists of synthetic resins offering outstanding punchability, high tool-life lubrication, and excellent interlaminar resistance. Recommended for medium and large electric motors where high stamping speeds are required.
C-5 / Inorganic & Chromate-Free Semi-Organic
Combines inorganic phosphate matrix with organic polymers. Formulated for high-heat stress-relief annealing ($750^\circ\text{C} - 850^\circ\text{C}$) without coating degradation or inter-lamination sticking. Environmental RoHS and REACH compliant.
Self-Bonding Varnish (Backlack Coating)
Advanced heat-activatable thermosetting resin pre-applied to CRNGO strip. Enables heat-bonded motor cores without welds, rivets, or interlocking tabs—completely eliminating parasitic eddy currents and operational acoustic vibration noise.
China Factory Efficiency & Global Commercial Sourcing Advantages
Why leading global motor, generator, and appliance manufacturers partner directly with our specialized Chinese steel manufacturing facilities.
Continuous Cold Rolling Precision
Our mill utilizes multi-stand tandem cold rolling lines equipped with dynamic Hydraulic Automatic Gauge Control (AGC) and laser thickness scanning. We maintain sub-micron strip thickness tolerances across the full width ($\pm 0.005\,\text{mm}$), eliminating motor stack height variations during automatic stamping assembly.
Integrated Molten Steel to Slitting Operations
By integrating hot coil selection from tier-1 steelmakers (Baosteel, Shougang, WISCO) directly into our automated pickling, cold rolling, continuous annealing, coating, and high-speed multi-blade slitting workshops, we reduce production lead times by over $45\%$ compared to standard distribution channels.
Burr-Free Precision Slitting Capability
Equipped with ultra-rigid carbide rotary shear knives, our slitting lines limit edge burr heights to under $0.015\,\text{mm}$. Minimal burrs prevent inter-laminar short circuits during rotor and stator lamination assembly, preserving nominal core efficiency.
Streamlined B2B Procurement & Scalable Capacity
As a specialized B2B non-grain oriented electrical steel supplier, our facilities handle monthly output volumes exceeding 100,000 metric tons. We accommodate master coil purchasing (weights from 3 to 10 MT), custom slit coils (widths from 15mm up to 1250mm), and cut-to-length sheet packs tailored for high-speed stamping presses (Schuler, Aida, Yamada Dobby).
- Factory Direct Wholesale Pricing: Eliminates middleman markups for competitive tender bidding.
- Strict Mill Test Verification: Full traceabilty with EN 10204 3.1 certification per coil heat number.
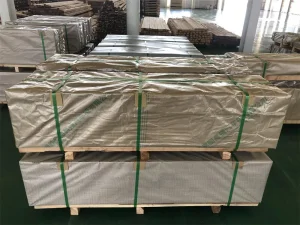
- Seaworthy Export Packaging: VCI anti-rust film, heavy-duty galvanized outer steel wrappers, eye-to-sky / eye-to-side wooden palletization.
Commercial Supply Contract Metrics
| Monthly Capacity | 100,000+ Metric Tons |
| Minimum Order Quantity (MOQ) | 5 MT per size (Trial orders flexible) |
| Thickness Tolerance | ±0.005 mm to ±0.01 mm |
| Slitting Width Tolerance | ±0.10 mm |
| Lead Time | 15 - 25 Days to FOB Tianjin / Shanghai |
Localized & Global Industrial Application Scenarios
From high-frequency electric vehicle powertrains to mega-watt industrial generators, CRNGO steel underpins modern electrification.
Electric Vehicle (EV) Traction Motors
Thin-gauge CRNGO (0.25mm - 0.35mm, M270-35A / 30WW270) provides low high-frequency core loss under high RPM inverter drive conditions (up to 20,000 RPM), boosting driving range and power density.
High-Efficiency Industrial Motors (IE3 / IE4 / IE5)
Standard and high-induction grades (M330-50A, M350-50A) optimized for continuous-duty pump, fan, conveyor, and industrial compressor systems, lowering life-cycle electricity consumption.
Hermetic HVAC & Appliance Compressors
Pre-coated silicon steel coils engineered for refrigeration and air-conditioning compressors requiring extreme mechanical cleanliness, burr control, and high torque output in sealed environments.
Hydro & Wind Power Generators
Heavy-duty stator punchings made from high magnetic permeability CRNGO sheets, maintaining high flux density ($B_{5000} \ge 1.68\,\text{T}$) to maximize megawatt electrical yield per ton of steel.
Global Market Trends & Next-Generation CRNGO Innovations
Strategic perspectives on decarbonization mandates, ultra-thin electrical steel development, and smart manufacturing trajectories.
1. Shift Toward Ultra-Thin Gauges (0.15mm - 0.20mm)
As motor speeds scale up in modern electric vehicles and high-speed aerospace actuators, excitation frequencies increase from 50Hz/60Hz to over 400Hz–1000Hz. Traditional 0.50mm sheets suffer excessive eddy current losses. The market is shifting rapidly toward ultra-thin 0.15mm and 0.20mm silicon steel, reducing high-frequency iron loss by up to $60\%$.
2. Self-Bonding Coating Revolution
Interlocking, welding, or bolting motor laminations creates inter-plate shorting paths that degrade core efficiency. Advanced self-bonding varnishes (Backlack) bond laminations under heat and pressure. This eliminates mechanical distortion, yields sub-micron gap precision, and reduces motor noise by up to 5 dB.
3. Decarbonization & Green Steel Compliance
With global carbon border adjustment mechanisms (such as EU CBAM) taking effect, global buyers demand low-carbon electrical steel. Chinese factories are integrating scrap-based Electric Arc Furnaces (EAF) and hydrogen-reduced iron (DRI) processes to lower Scope 1 and Scope 2 carbon intensity per ton of finished silicon steel.
CRNGO Technical Roadmap & Performance Progression
Global Buyer Procurement Framework & Quality Inspection Standard
A rigorous quality assurance protocol designed to eliminate dimensional, magnetic, and mechanical defects in wholesale silicon steel shipments.
1. Epstein Frame Magnetic Testing
Every heat and master coil undergoes standardized Epstein frame testing (IEC 60404-2) or single-sheet tester (SST) protocols to verify specific loss ($P_{1.5/50}$) and magnetic induction ($B_{5000}$) prior to mill release.
2. Dimensional Profile & Crown Control
Precision micrometers and continuous laser thickness sensors ensure transverse thickness crown profile is kept below $0.004\,\text{mm}$, ensuring flat, uniform stamping without wave edges or center buckles.
3. Coating Adhesion & Insulation Resistance
Insulation coatings undergo scratch resistance, Franklin insulation testing (ASTM A717), and bend testing (Franklin value > 50 $\Omega\cdot\text{cm}^2/\text{lamination}$) to guarantee no flaking during die stamping.
Heavy-Duty Export Packaging Standard for Silicon Steel Coils
Silicon steel is highly sensitive to moisture and edge impact damage. Our factory enforces a multi-layer ocean export packaging protocol:
Technical & Commercial FAQ for Silicon Steel Buyers
Expert engineering answers to critical purchasing, metallurgical, and manufacturing questions.
What is the core difference between CRNGO and CRGO silicon steel?
How does silicon content affect the mechanical and magnetic performance of electrical steel?
Is stress-relief annealing (SRA) necessary after lamination stamping?
What thickness tolerance and slit width tolerances can your factory maintain?
Which insulation coating (C-3 vs C-5) should I specify for motor laminations?
What mill test certificates and quality documents are supplied with wholesale orders?
Additional Industrial Steel & Pipe Line Items
Showing 9 - 16 of Factory Direct Line Items



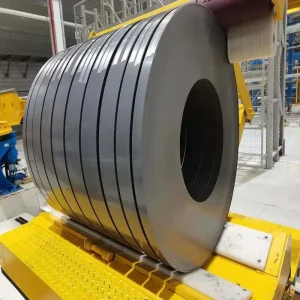

Request Mill-Direct Silicon Steel Quotes & Technical Data Sheets
Partner with a trusted Chinese electrical steel manufacturer. Connect with our senior metallurgical engineers for custom slit widths, coating selection, or volume price quotations.
Contact Our Export Engineering Team