
Featured Industrial Steel Offerings
Mill-direct export grade silicon steel, galvanized structural pipes, stainless coils, and specialized industrial steel products.





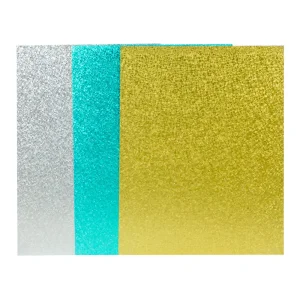


Technical Core: What Makes CRGO Essential for Transformer Cores?
An in-depth metallurgical analysis of grain orientation, Goss texture optimization, domain refinement, and core loss physics.
Crystallographic Alignment
Cold Rolled Grain Oriented (CRGO) silicon steel achieves high magnetic permeability along the rolling direction through precise secondary recrystallization. This creates the Goss texture (110)[001], aligning iron crystals so magnetic domain orientation experiences minimal reluctance during transformer magnetization cycles.
Laser Scribing & Plasma Treatment
Advanced CRGO grades undergo domain refinement via laser etching or mechanical scratching. This subdivides main magnetic domains into narrower sub-domains, significantly reducing anomalous eddy current losses ($P_a$) at operating frequencies of 50Hz and 60Hz without degrading high flux density stability.
Carlite Phosphate Coating
Our CRGO coils feature an inorganic phosphate insulation coating (IEC 60404-1-1 Class C-5). This layer imparts high interlaminar resistance (>100 $\Omega\cdot\text{cm}^2$), withstands stress-relief annealing temperatures up to 820°C, and induces tensile stress to further suppress magnetic core loss.
Why Global OEMs Procure Wholesale CRGO Steel from China Factories
China has established the world's most integrated, technologically advanced manufacturing ecosystem for electrical steel production and transformer core processing.
1. Fully Integrated Metallurgy to Slitting
From initial iron ore reduction and vacuum degassing to 20-high Sendzimir cold rolling and continuous annealing, Chinese mills operate seamless, end-to-end quality loops. Factory direct sourcing eliminates intermediary markups and guarantees complete heat-traceability via digital Mill Test Certificates (MTC EN 10204 3.1).
2. Ultra-Precise Width & Burr Tolerances
Modern transformer core fabrication demands precise strip slitting. Chinese slitting facilities utilize carbide rotary shears capable of maintaining width tolerances within $\pm0.05\text{ mm}$ and edge burr heights below $0.02\text{ mm}$, preventing inter-lamination short circuits and minimizing no-load transformer losses.
3. Unmatched Economies of Scale
Housing over 60% of the world's silicon steel rolling capacity, Chinese factories provide reliable high-volume order fulfillment. Flexible production scheduling allows global procurement teams to secure customized coil weights (2.0 MT to 5.0 MT) and tailored width specifications with standard 15 to 25-day lead times.
Global Industry Trends & Efficiency Directives Impacting CRGO Sourcing
Strict energy efficiency regulations worldwide are forcing electrical grid operators and transformer OEMs to upgrade core material specifications.
| Region / Standard | Efficiency Mandate | Target Loss Standard | Recommended CRGO Grade Specification |
|---|---|---|---|
| European Union (EU Ecodesign Tier 2) | EN 50588-1 / EN 50708 | Strict No-Load Loss ($P_0$) Reduction | High-Permeability (Hi-B) Laser Etched 0.20mm - 0.23mm (e.g., 20QG080, 23QG085) |
| United States (US DOE 2026 Mandate) | 10 CFR Part 431 Efficiency Standards | Substantial $P_0$ & $P_k$ Reductions | Domain Refined Hi-B 0.23mm - 0.27mm (e.g., 23NV085, 27NV090) |
| India (BIS / BEE Standards) | IS 1180 (Part 1) Star Rating | Star 3 to Star 5 Energy Ratings | Conventional & Hi-B CRGO 0.23mm - 0.30mm (e.g., 23Q100, 27Q110, 30Q120) |
| China (GB 20052-2020) | Level 1 & Level 2 Energy Efficiency | Ultra-Low No-Load Loss Profile | Laser-Scribed Ultra-Thin 0.18mm - 0.20mm (e.g., 18QG075, 20QG080) |
Localized Application Scenarios & Selection Matrix
Selecting the optimal CRGO steel thickness and magnetic grade based on transformer topology, operating environment, and total ownership cost calculations.
Oil-Immersed Distribution Units (10kV - 35kV)
Distribution transformers run continuously under varying loads. Standard 0.23mm to 0.27mm CRGO coils (e.g., 23Q090, 27Q100) offer an ideal balance of low hysteresis loss, excellent core stacking performance, and total cost optimization.
Large Power Transformers (110kV - 750kV)
Ultra-High Voltage (UHV) power step-up units demand maximum magnetic induction and minimal heat buildup. High-Permeability Hi-B CRGO (0.20mm - 0.23mm) provides maximum saturation induction without thermal degradation, lowering cooling oil circulation demand.
Cast Resin Dry-Type Transformers
Installed in commercial high-rises and data centers where acoustic noise controls are mandatory. Domain-Refined CRGO suppresses magnetostriction, reducing transformer humming noise by up to 3 dB to 8 dB compared to non-refined core materials.
Complete Quality Assurance Lifecycle & Global Logistics
How our factory mitigates global supply risks through rigorous testing, seaworthy packaging, and transparent quality documentation.
1. Epstein Frame Testing
Every master coil undergoes Epstein frame testing according to IEC 60404-2 to measure magnetic loss ($P_{1.7/50}$) and AC magnetic permeability ($B_{8000}$) prior to slitting release.
2. Thickness Uniformity Checks
Continuous online X-ray thickness gauges monitor cold rolling tolerances, ensuring transverse and longitudinal variations remain under $\pm0.005\text{ mm}$ across the entire coil width.
3. VCI Corrosion Inhibitor Wrap
Slit CRGO coils are sealed with Volatile Corrosion Inhibitor (VCI) film, heavy-duty metallic edge protectors, and corrugated steel outer wrapping to prevent sea-salt humidity damage.
4. Ocean Freight Rigging
Eye-to-side or eye-to-sky coils are anchored on reinforced wooden/steel pallets designed to sustain 20GP container motion without physical edge deformation.
Technical & Sourcing FAQ
Comprehensive answers to common engineering, metallurgical, and commercial procurement inquiries.
What is the fundamental difference between CRGO and CRNGO silicon steel?
CRNGO (Cold Rolled Non-Grain Oriented) steel exhibits isotropic magnetic properties in all directions, making it essential for rotating electrical machinery like electric motors, generators, and armatures where magnetic field orientation changes continuously.
How does thickness affect core loss in CRGO transformer laminations?
Reducing sheet thickness from 0.30mm down to 0.20mm or 0.18mm dramatically lowers eddy current circulation within the lamination, lowering overall no-load losses in high-efficiency transformers.
Why is stress-relief annealing necessary after cutting or slitting CRGO steel?
Stress-relief annealing in a protective nitrogen atmosphere at 780°C - 820°C for 2 to 3 hours restores the distorted crystal structure, recovering the material's original low-loss magnetic profile.
What are the key standard international equivalents for CRGO steel grades?
- 0.23mm Hi-B Grade: 23QG085 (GB) ≈ M085-23P (EN) ≈ 23NV085 (ASTM) ≈ NV23P-85 (JIS)
- 0.27mm Conventional Grade: 27Q110 (GB) ≈ M110-27S (EN) ≈ 27H110 (ASTM) ≈ 27G110 (JIS)
- 0.30mm Conventional Grade: 30Q120 (GB) ≈ M120-30S (EN) ≈ 30H120 (ASTM) ≈ 30G120 (JIS)
What key information should be provided when requesting a wholesale CRGO quote?
- Specific Grade or Core Loss Specification: (e.g., 23QG085, 27Q100, or maximum $P_{1.7/50}$ limit).
- Form Factor & Dimensions: Master coils, slit coils (width tolerance), or pre-cut cut-to-length / step-lap transformer laminations.
- Coil ID & Max Weight Limits: Standard 508mm ID with target coil package weights (e.g., 2.5 MT max).
- Insulation Coating Requirement: Standard Carlite coating (IEC Class C-5) or specialized high-temperature resistant coating.
- Order Volume & Destination Port: For accurate CIF ocean freight calculations.
Complementary Factory Direct Steel Series
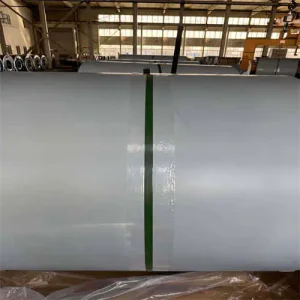
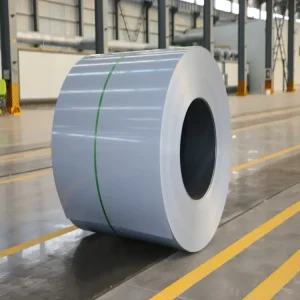
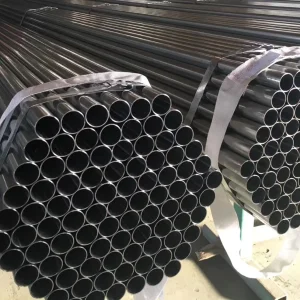
Explore our complete catalog of industrial steel pipes, stainless steel coils, solar structural sheets, and steel fittings.


Partner with China's Premier CRGO & Steel Core Manufacturer
Need custom slitting tolerances, certified low-loss electrical steel grades, or mill-direct pricing for upcoming transformer production schedules? Our metallurgical export team provides 24-hour quotation responses.