
Featured Cold Rolled & Electrical Silicon Steel Coils
Direct mill shipments, fully certified CRNGO coils, stainless steel, and specialty industrial metal solutions for global distributors and OEMs.




Executive Summary: Global Macro Industrial Shift in CRNGO Silicon Steel
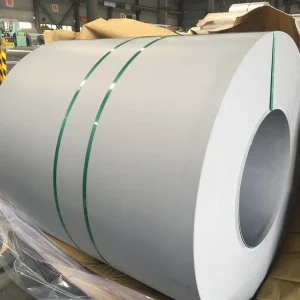
The global transition toward high-efficiency electromechanical systems, driven by decarbonization mandates, the rapid proliferation of Electric Vehicles (EVs), and mandatory energy efficiency standards (IE3, IE4, IE5 under IEC 60034-30-1), has created an unprecedented structural demand for advanced magnetic materials. At the epicenter of this technological transformation are Cold Rolled Non-Grain Oriented (CRNGO) Silicon Steel Coils. Engineered specifically to exhibit isotropic magnetic properties—delivering identical magnetic permeability in all spatial directions within the rolling plane—CRNGO electrical steel represents the core electromagnetic medium for rotating electrical machinery, power distribution systems, and hermetic compressor units globally.
Technical Insight: Unlike Cold Rolled Grain-Oriented (CRGO) steel, which optimizes magnetic flux along a single longitudinal direction for static transformers, CRNGO features a randomized or tailored crystallographic texture (predominantly {100} cubic texture) critical for rotating armatures, stators, and rotors subjected to continuously shifting magnetic vectors.
As global tier-1 original equipment manufacturers (OEMs) and electrical steel stampers navigate volatile supply chains, finding verified wholesale cold rolled non grain oriented steel coils suppliers & factory partners has evolved from a standard procurement task into a high-stakes strategic imperative. Fluctuations in raw material quality, thickness variations, magnetic core loss ($P_{1.5/50}$), and interlamination resistance directly impact motor efficiency ratings and thermal performance.
Modern electrical engineering demands tight dimensional tolerances, superior strip flatness, low edge burr formation during high-speed stamping, and advanced surface insulation coatings (C-3, C-5, C-6 class). Sourcing directly from certified mill suppliers guarantees that chemical formulations—specifically silicon content ranging from 1.0% to 3.5% combined with micro-alloyed aluminum and manganese—are precisely calibrated to balance electrical resistivity, magnetic induction ($B_{50}$), and mechanical rollability.
Engineering Fundamentals of CRNGO Electrical Steel Coils
To evaluate CRNGO steel performance, procurement directors and engineering leads must look beyond surface dimensions and understand the underlying physics of ferromagnetic materials. Core loss, magnetic polarization, grain boundary engineering, and insulation resistance represent the primary metrics dictating component performance.
1. Microstructure, Chemical Composition & Alloying Metallurgy
Non-grain oriented silicon steel relies on a high-purity iron matrix alloyed primarily with Silicon (Si) and Aluminum (Al). Silicon elevates electrical resistivity, effectively attenuating dynamic eddy current losses ($P_e$) generated when alternating magnetic fields induce circulating currents within core laminations. However, excessive silicon (>3.8 wt.%) induces severe lattice brittleness, compromising cold rolling feasibility.
- Silicon Content (1.0% – 3.5%): Higher silicon content yields lower core loss (e.g., M310, M350) required for high-efficiency motors, whereas lower silicon content enhances mechanical strength and magnetic induction at saturation ($B_{50}$) for cost-sensitive standard applications (e.g., M600, M800).
- Aluminum Addition (0.2% – 1.0%): Aluminum acts synergistically with silicon to boost electrical resistivity while refining the grain structure during continuous annealing protocols.
- Ultra-Low Impurity Limits: Elements like Carbon (C ≤ 0.005%), Sulfur (S ≤ 0.005%), Nitrogen (N ≤ 0.005%), and Oxygen must be strictly minimized to prevent domain wall pinning and premature magnetic aging.
2. Core Loss Breakdown: Hysteresis vs. Eddy Current vs. Anomalous Loss
Total magnetic core loss ($P_t$) within CRNGO laminations operating at a magnetic flux density $B$ and frequency $f$ is mathematically dissected into three distinct physics-based components:
Core Loss Equation: $P_t = P_h + P_e + P_a = k_h \cdot f \cdot B^n + k_e \cdot d^2 \cdot f^2 \cdot B^2 + P_a$
Where $P_h$ represents hysteresis loss, $P_e$ is classical eddy current loss, $P_a$ is anomalous loss, $d$ is lamination thickness, and $k_h, k_e$ are material physical coefficients.
Reductions in lamination thickness (from 0.50mm down to 0.35mm or 0.20mm) yield a quadratic drop in classical eddy current loss ($d^2$), making thinner CRNGO strip indispensable for high-frequency traction motors operating above 400 Hz.
3. Standard CRNGO Grade Specifications & Technical Comparison
The standard classification under IEC 60404-8-4, EN 10126, and JIS C2552 establishes strict limits for maximum core loss at 1.5 Tesla / 50 Hz ($P_{1.5/50}$) and minimum magnetic induction at 5000 A/m ($B_{50}$). Below is a authoritative comparative matrix of primary CRNGO mill grades supplied globally:
| Steel Grade (IEC / EN) | Nominal Thickness (mm) | Max Core Loss $P_{1.5/50}$ (W/kg) | Max Core Loss $P_{1.5/60}$ (W/kg) | Min Magnetic Flux $B_{50}$ (Tesla) | Typical Silicon Content (%) | Primary Industrial Applications |
|---|---|---|---|---|---|---|
| M310-35A | 0.35 | 3.10 | 2.40 | 1.60 | 3.0 - 3.3% | EV Traction Motors, High-RPM Motors |
| M350-50A | 0.50 | 3.50 | 2.70 | 1.62 | 2.8 - 3.1% | IE4 Premium Efficiency Motors, Pumps |
| M470-50A | 0.50 | 4.70 | 3.60 | 1.64 | 2.2 - 2.5% | Standard Industrial Motors, HVAC Compressors |
| M600-50A | 0.50 | 6.00 | 4.60 | 1.66 | 1.5 - 1.8% | Home Appliances, Small Fractional HP Motors |
| M800-64A | 0.64 | 8.00 | 6.10 | 1.68 | 1.0 - 1.3% | Ballasts, General Electromagnetic Actuators |
4. Surface Insulation Coating Technologies (C-3, C-5, C-6)
Untreated laminations risk high interlamination circulating currents that cause catastrophic core overheating. Modern cold rolling factories apply ultra-thin (0.5 to 3.0 μm) organic, inorganic, or semi-organic insulation coatings during final continuous annealing:
C-3 Organic Coating
Composed of organic resin formulations. Delivers exceptional punchability, extending progressive stamping die life up to 1,000,000 strokes. Ideal for small, low-temperature motors where burn-out annealing is not required.
C-5 Semi-Organic Inorganic Coating
Combines inorganic phosphates/chromates with organic additives. Excellent heat resistance (withstanding stress-relief annealing up to 750°C in protective atmospheres) alongside high interlamination resistance (> 50 Ω·cm²/lamina).
C-6 High-Inorganic Structural Coating
Formulated with high inorganic content for maximum breakdown voltage insulation, chemical oil immersion stability, and fire retardancy. Specially engineered for large power generators and hermetic oil-filled compressor units.
Global Market Dynamics & Supply Chain Economics
The global sourcing landscape for wholesale cold rolled non grain oriented steel coils is characterized by concentrated manufacturing expertise. Production of prime-grade CRNGO requires advanced industrial metallurgy, high-precision tandem cold rolling mills equipped with Automatic Gauge Control (AGC), high-temperature hydrogen continuous annealing furnace lines, and automated online laser thickness inspection.
Key Market Drivers Shaping Wholesale Sourcing:
- Mandatory Energy Efficiency Standards: Regulatory frameworks such as the European Union's Ecodesign Directive (EU 2019/1781) and China's GB 18613-2020 have rendered older, high-loss motor designs obsolete. Manufacturers must transition to high-grade CRNGO (M270, M310, M350) to meet IE3 and IE4 efficiency thresholds.
- Electric Vehicle (EV) Powertrain Escalation: EV traction motors require ultra-thin, low-loss CRNGO laminations capable of operating at elevated frequencies (400 Hz to 1,200 Hz) and rotational speeds exceeding 15,000 RPM. This shift has strained global production capacities for high-frequency thin-gauge steel (0.20mm – 0.35mm).
- Shift Toward Direct Mill Sourcing: Tier-1 motor fabricators are bypassing secondary trading intermediaries. Contracting directly with integrated suppliers and production factories secures consistent batch-to-batch chemical homogeneity, guaranteed slit-edge tolerances (±0.1mm), and customized coil package weights tailored to automatic decoiling lines.
Supply Chain Advantage: Direct factory partnerships allow global buyers to specify custom coil slitting, tailored surface coating weights, special oiled or VCI anti-rust protective packaging, and flexible order minimums (MOQs) necessary for scaling project production.
Localized Industrial Application Scenarios
CRNGO electrical steel coils serve as the core functional building block across diverse global industries. Sourcing the optimal steel grade directly determines end-product electrical thermal limits, acoustic noise levels, and energy efficiency ratings.
EV Traction Motors & Auxiliary Drives
Traction motors require low magnetic hysteresis loss and exceptional tensile yield strength (> 420 MPa) to withstand centrifugal stresses on high-speed rotors. Thin-gauge CRNGO grades (M250-35A, M270-35A) minimize rotor iron loss, directly extending vehicle driving range per charge cycle.
Heavy Machinery & IE3/IE4 Motors
Industrial induction motors, hydraulic pump drives, and ventilation blowers utilize standard 0.50mm CRNGO grades (M350-50A, M470-50A). High magnetic permeability at operating induction (1.5 T) reduces magnetizing current requirements, raising overall efficiency while lowering thermal dissipation.
Hermetic Inverter Compressors
Air conditioning and commercial refrigeration compressors demand variable-speed operation under variable frequencies. High-permeability CRNGO with C-5 surface coating prevents chemical degradation in hot refrigerant and oil environments, ensuring long compressor operational lifespans.
Renewable Energy Generators
Direct-drive wind turbine generators and hydro-electric power alternators require large-diameter stator core laminations stamped from high-grade CRNGO. Superior magnetic uniformity eliminates localized magnetic saturation, dampening acoustic vibration and electromagnetic hum.
Home Appliance Drives
Washing machine drum motors, refrigerator compressors, and dishwasher circulation pumps rely on cost-optimized CRNGO grades (M600-50A, M800-50A). These offer superior punchability for high-volume automated stamping lines while meeting standard energy labels.
Small Transformers & Reactors
While primary grid transformers utilize grain-oriented steel, low-power control transformers, welding equipment, magnetic chokes, and line reactors utilize non-grain oriented steel due to complex core geometries and isotropic flux requirements.
Quality Control Protocols, Standards Compliance & Mill Certification
Delivering high-reliability cold rolled non grain oriented electrical steel coils requires meticulous factory-level quality engineering. Substandard silicon steel leads to catastrophic punching burrs, coating flaking, localized thermal runaway, and premature motor failure.
1. Global Compliance Standards Framework
Leading wholesale suppliers manufacture and test CRNGO steel coils in strict accordance with international standards:
- IEC 60404-8-4: Magnetic materials – Specification for individual materials – Cold-rolled non-oriented electrical steel sheet and strip delivered in the fully-processed state.
- ASTM A683 / A683M: Standard Specification for Nonoriented Electrical Steel, Fully Processed Types.
- JIS C 2552: Cold-rolled non-oriented electrical steel strips and sheets.
- EN 10126: Cold rolled non-oriented electrical steel sheet and strip delivered in the fully-processed state.
2. Comprehensive Factory Inspection & Testing Protocols
Prior to dispatch, every master coil undergoes rigorous testing at state-of-the-art mill laboratories, backed by EN 10204 3.1 Certified Mill Test Reports (MTRs):
| Inspection Stage | Testing Method / Equipment | Target Quality Parameter | Engineering Tolerance Limit |
|---|---|---|---|
| Magnetic Testing | Epstein Frame / Single Sheet Tester (SST) | Core Loss ($P_{1.5/50}$), Magnetic Induction ($B_{50}$) | Strictly within standard grade guaranteed max/min |
| Dimensional Gauge | Non-Contact Isotope X-Ray Gauge | Strip Thickness Uniformity & Crown Tolerance | ± 0.015 mm across longitudinal/transverse width |
| Slitting Quality | Optical Laser Micrometer Edge Scanner | Edge Burr Height & Camber Deviation | Burr Height ≤ 0.02 mm; Camber ≤ 1.0 mm/2000 mm |
| Coating Inspection | Franklin Insulation Tester / Cross-Hatch Adhesion | Interlamination Resistance & Coating Adhesion | Resistance > 30 Ω·cm²/lamina; Class 0 flaking rating |
| Mechanical Testing | Tensile Testing Machine / Micro-Vickers Hardness | Yield Strength, Tensile Strength, Elongation | Optimized for high-speed stamping die compatibility |
3. Export Packaging & Global Logistics Assurance
Electrical steel is highly vulnerable to atmospheric humidity, sea-freight condensation, and handling deformation. Reliable factory suppliers utilize heavy-duty export packaging standards: custom steel eye-to-sky or eye-to-wall coil skids, double-layer Volatile Corrosion Inhibitor (VCI) anti-rust paper, full outer metallic galvanized steel wrapping, and heavy-duty steel radial/circumferential strapping.
Technical Roadmap & Future Outlook (2025–2035)
The electrical steel sector is experiencing accelerated technological evolution. As global energy frameworks mandate higher operational efficiencies and electrify transportation, CRNGO manufacturing is advancing along three primary technological vectors:
1. Ultra-Thin Gauges (≤ 0.15mm - 0.20mm)
Driven by ultra-high-speed traction motors (>20,000 RPM) and aerospace high-frequency alternators, mill research focuses on commercializing 0.15mm and 0.20mm ultra-thin CRNGO. These gauges drastically attenuate dynamic high-frequency eddy current losses, unlocking elevated motor RPM efficiencies.
2. Self-Bonding Varnish Coatings (Backlack)
Traditional interlocking, riveting, or welding of stator stack laminations induces mechanical stresses that degrade local magnetic properties. Next-generation CRNGO coils feature heat-activated self-bonding coatings (Backlack). Once stamped and heated, laminations fuse seamlessly into a rigid core, optimizing magnetic flux, eliminating acoustic noise, and optimizing heat dissipation.
3. Decarbonized "Green Steel" Production
Global OEMs are prioritizing low-carbon supply chain footprints. Leading electrical steel mills are transitioning to Direct Reduced Iron (DRI) powered by green hydrogen, combined with Electric Arc Furnaces (EAF) utilizing 100% renewable energy. Purchasing green-certified CRNGO coils assists OEMs in fulfilling Scope 3 carbon reduction pledges.
Frequently Asked Questions (Technical Sourcing Q&A)
Comprehensive engineering and procurement answers regarding wholesale cold rolled non grain oriented steel coils procurement, specifications, and applications.
Explore Additional Wholesale Steel & Industrial Products
Complete product line coverage directly from our certified manufacturing mills in Tianjin, China.





Initiate Your Wholesale CRNGO Steel Order Today
Connect directly with our engineering metallurgy team. Request mill certificates, technical data sheets, custom slitting width quotes, and trial shipment schedules tailored to your OEM production line.