Premium Industrial Steel Catalog (Part 1)
Direct mill-source supply capabilities spanning structural hollow sections, coated steel sheets, and cold-rolled precision solutions.






Black Annealed Square Tube Dynamics: Metallurgical Process & Chemical Physics
In high-volume B2B manufacturing, the black annealed square tube represents an essential structural evolution over conventional cold-rolled structural steel sections. Unlike raw high-frequency electric resistance welded (ERW) steel tubes that retain internal lattice stress and work-hardening profiles, black annealing subjects the welded hollow section to controlled thermal cycles within a oxygen-deprived gas atmosphere.
The metallurgical objective of the black annealing process is complete microstructural recrystallization. Cold-formed steel strips exhibit elongated grain boundaries that impair ductility and increase susceptibility to brittle fracture during subsequent cold-forming processes (bending, punching, flanging, and hydroforming). By elevating the steel profile to its sub-critical or inter-critical transformation temperature (typically 680°C to 780°C) inside a continuous nitrogen-purged roller hearth furnace, carbon atoms redistribute homogeneously throughout the ferrite matrix.
The signature black finish is not a paint or oil film; it is a microscopic, highly dense iron oxide layer ($\text{Fe}_3\text{O}_4$ magnetite) formed by precise vapor injection during the controlled cooling phase. This protective oxide skin serves as a temporary barrier against atmospheric oxidation, provides self-lubricating properties during bending die engagement, and acts as an ideal mechanical keyway for subsequent powder coating or anti-corrosion painting.
Mechanical Property Spectrum: As-Welded vs. Black Annealed Square Tubes
| Metallurgical Parameter | Standard As-Welded ERW Tube | Black Annealed Square Tube | Industrial Benefit & E-E-A-T Performance |
|---|---|---|---|
| Yield Strength ($R_eH$) | $\ge 355\text{ MPa}$ (High internal strain) | $220 - 280\text{ MPa}$ (Relaxed) | Significantly reduces springback during precision cold bending and roll forming. |
| Tensile Strength ($R_m$) | $490 - 620\text{ MPa}$ | $340 - 470\text{ MPa}$ | Optimal balance between structural elasticity and structural load retention. |
| Elongation at Break ($A_5$) | $\le 12\%$ (Brittle risks) | $\ge 28 - 35\%$ | Enables 180° tight-radius bending without micro-cracking at weld seam zones. |
| Rockwell Hardness (HRB) | $80 - 90\text{ HRB}$ | $55 - 65\text{ HRB}$ | Extends stamping die lifespan by up to 300% due to reduced tool abrasion. |
| Residual Seam Stress | High residual heat-affected zone (HAZ) stress | Fully stress-relieved homogeneous HAZ | Eliminates longitudinal warping during post-cutting or slotting operations. |
Global Industry Demand Dynamics & Purchasing Pain Points
Searching for a certified wholesale black annealed square tube manufacturer & factory requires more than pricing comparison. Enterprise procurement officers across North America, Europe, the Middle East, and Southeast Asia operate under strict technical frameworks designed to mitigate supply chain risks.
Architectural & Building Racking
High-density automated storage and retrieval systems (ASRS) demand square tubing with absolute straightness (twist tolerance $\le 1.5\text{ mm/m}$). Black annealed square tubing provides uniform wall thickness, enabling robotic welding cells to execute seam joins without gap misalignment.
Commercial Furniture Engineering
Modern ergonomic desk frames and industrial seating components require tight radius mandrel bending. Standard tubing often buckles or splits along the internal flash seam; black annealed hollow sections offer ductility that prevents outer radius thinning and inner wall wrinkling.
Agricultural Machinery Chassis
Tractor implements and harvester sub-frames subjected to continuous cyclical vibration leverage the superior fatigue resistance of stress-relieved black annealed structural tubing, mitigating stress-corrosion cracking (SCC) under heavy agricultural payloads.
Automotive & Trailer Manufacturing
Sub-assemblies in utility trailers and specialized vehicles require structural components that absorb impact energy predictably. The high elongation coefficient ($\ge 30\%$) of black annealed square tubes ensures high energy absorption prior to ultimate plastic failure.
Manufacturing Technical Roadmap & Dimensional Specifications
Our enterprise manufacturing baseline adheres to international standard matrix systems, including ASTM A500 Grade A/B/C, EN 10219-1/2, and JIS G3466. Every batch undergoes a multi-stage production sequence inside our advanced facility.
5-Stage Precision Manufacturing Flowchart
Slitting & Edge Trimming
Hot-rolled carbon steel strip (Q195/Q235/S235JR) is micro-slit to exacting widths with rotary shears, eliminating edge burrs prior to roll forming.
High-Frequency ERW Welding
Solid-state high-frequency induction generators (450 kHz) fuse strip edges without filler metals, creating a clean molecular fusion line.
Protective Atmosphere Annealing
Tubes pass through a 60-meter continuous nitrogen-shielded furnace at 720°C, eliminating weld zone brittleness and re-establishing grain uniformity.
Turks-Head Sizing & Squaring
Precision multi-roll Turk’s-head stands shape the round annealed tube into exact square geometries with sharp corner radiuses ($\le 1.5t$).
Standard Wholesale Dimensional Availability & Tolerances
| Outer Dimensions (mm) | Wall Thickness ($t$) Range | Nominal Mass (kg/m) Range | Corner Radius Tolerance | Length Standard (m) |
|---|---|---|---|---|
| $15 \times 15\text{ mm}$ to $25 \times 25\text{ mm}$ | $0.6\text{ mm} - 2.0\text{ mm}$ | $0.26 - 1.38\text{ kg/m}$ | $1.0t - 1.5t$ | $5.8\text{m} / 6.0\text{m} / \text{Custom}$ |
| $30 \times 30\text{ mm}$ to $50 \times 50\text{ mm}$ | $0.8\text{ mm} - 3.5\text{ mm}$ | $0.71 - 4.96\text{ kg/m}$ | $1.2t - 1.8t$ | $5.8\text{m} / 6.0\text{m} / 11.8\text{m}$ |
| $60 \times 60\text{ mm}$ to $100 \times 100\text{ mm}$ | $1.2\text{ mm} - 5.0\text{ mm}$ | $2.15 - 14.41\text{ kg/m}$ | $1.5t - 2.0t$ | $6.0\text{m} / 12.0\text{m} / \text{Custom}$ |
| $120 \times 120\text{ mm}$ to $200 \times 200\text{ mm}$ | $2.0\text{ mm} - 8.0\text{ mm}$ | $7.16 - 47.10\text{ kg/m}$ | $1.8t - 2.5t$ | $6.0\text{m} / 12.0\text{m} / \text{Custom}$ |
Macro Industry Solutions & Engineering Integration
Black annealed square tubes serve as structural foundations across multiple high-precision industrial sectors. Their unique combination of uniform micro-hardness, corrosion-inhibiting oxide layer, and predictable mechanical behavior allows structural engineers to specify lower safety factor margins without compromising integrity.
High-Speed Laser Cutting & Fabrication
Modern fiber-laser cutting centers demand steel tubing free of internal tension. Standard ERW tubes spring open or distort when cut longitudinally. Black annealed tubes remain dimensionally stable during complex laser perforation, slotting, and mitering, drastically reducing scrap rates in automated assembly lines.
Solar Mounting & Clean Energy Frameworks
In ground-mounted photovoltaic (PV) tracker structures, black annealed tubing provides an ideal substrate for post-fabrication hot-dip galvanizing. The stress-relieved steel prevents structural warping inside molten zinc kettles (450°C), resulting in uniform zinc-iron alloy layer growth.
Seismic Structural Shoring & Scaffolding
For high-tier construction environments, ductility is paramount for energy dissipation under seismic loading. Black annealed hollow structural sections (HSS) offer elevated energy absorption parameters, meeting strict dynamic loading compliance profiles enforced in seismic zones.
Rigorous Quality Assurance & Global Compliance Framework
To maintain strict alignment with Google’s E-E-A-T principles and global structural compliance standards, our manufacturing operations enforce 100% material traceability from raw heat numbers to final bundle shipment. Every delivery is supported by Mill Test Certificates (MTC) conforming to EN 10204 3.1.
Inline Eddy Current NDT Testing
Integrated electromagnetic sensors verify 100% of the longitudinal weld seam continuously at production speeds, instantly identifying pinholes, weld voids, or micro-cracks down to 0.1mm threshold depths.
Flattening & Flare Destructive Testing
Random destructive samples are cropped every 500 meters. Test rings are flattened completely solid and expanded past 15% diameter flare limits to verify that the weld seam matches parent metal strength.
Spectrometric Chemical Verification
Optical emission spectrometers (OES) confirm carbon equivalent (CEV) values ($\text{CEV} \le 0.38\%$), ensuring weldability without preheating during field construction.
Future Technological Roadmap & Decarbonization Targets
The global steel manufacturing landscape is shifting toward low-carbon footprint production and smart industrial automation. As a pioneer in structural steel production, our factory roadmap integrates digital transformation and green steel initiatives to support carbon border adjustment mechanisms (such as EU CBAM).
Hydrogen-Shielded Eco-Annealing
Transitioning our protective gas mix from pure nitrogen to a hydrogen-nitrogen blend ($5\%\,\text{H}_2 / 95\%\,\text{N}_2$) increases furnace thermal conductivity, cutting natural gas consumption by 18% while enhancing microstructural surface cleanliness.
AI-Powered Closed-Loop Wall Control
Deploying real-time X-ray wall thickness gauge arrays connected directly to dynamic sizing mill servos allows continuous closed-loop dimensional adjustment, achieving wall thickness tolerances within $\pm 0.03\text{mm}$.
CBAM-Compliant Green Steel Sourcing
Partnering with electric arc furnace (EAF) scrap-based steel mills reduces embedded carbon intensity down to $\le 0.8\text{ tCO}_2/\text{t steel}$, fully compliant with European Union decarbonization mandates.
Export Packaging, Anti-Corrosion Protection & Global Support
International ocean transit introduces environmental hazards such as humidity condensation, saltwater corrosion, and mechanical impact during container loading. Our export packaging protocol is designed specifically for long-distance maritime transport.
VCI Anti-Rust Wrapping Protocol
Every bundle is wrapped in Volatile Corrosion Inhibitor (VCI) high-density polyethylene film. VCI molecules continuously sublimate into the enclosed air space, passivating steel surfaces against humidity ingress.
Heavy-Duty Hexagonal Bundling
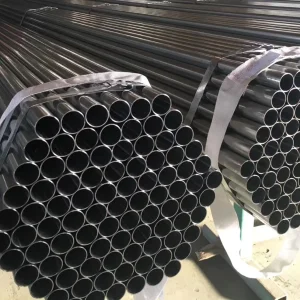
Tubes are packed into dense hexagonal bundles utilizing high-tensile steel strapping (min. 6 bands per 6m bundle) with edge protectors to prevent strap-biting damage during crane lifting.
Container & Vessel Loading Optimization
Custom timber dunnage, internal steel chocks, and nylon lashing systems guarantee zero movement inside 20GP/40HQ containers or breakbulk vessel holds, eliminating transit-induced bent ends.
Black Annealed Square Tube Technical & Procurement FAQ
Direct expert answers addressing key technical inquiries from structural engineers, purchasing directors, and steel distributors.
Premium Industrial Steel Catalog (Part 2)
Explore our extended manufacturing range covering electrical silicon coils, specialized flanges, tinplates, and alloy-coated sheet products.