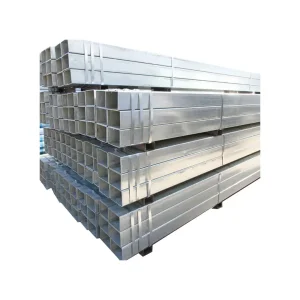
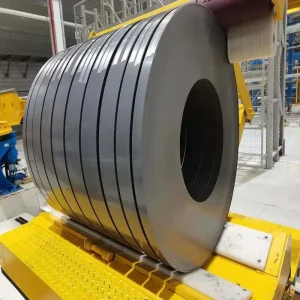
Featured Coated Steel & Structural Products
Explore our top-tier flat-rolled steel, ZM/AZM coated sheets, and custom structural tubes directly manufactured from our Tianjin mill facilities.




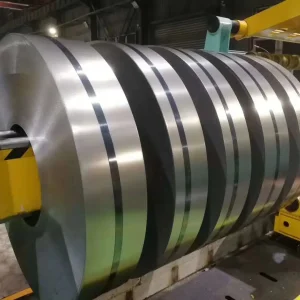
Metallurgical Mechanisms & The Self-Healing Edge Advantage
Zinc-Aluminum-Magnesium (Zn-Al-Mg / ZM / AZM) coated steel represents a paradigm shift in surface engineering technology. By integrating Magnesium (1.5% - 3.0%) and Aluminum (1.5% - 11.0%) into the traditional molten zinc bath, a highly stable ternary eutectic crystalline microstructure is established.
Ternary Eutectic Matrix
Unlike standard galvanized steel ($GI$) composed purely of soft zinc, Zn-Al-Mg coatings form a complex multi-phase matrix consisting of $Zn$, $Zn_2Mg$, and $Al$ binary/ternary phases. This dense physical structure dramatically lowers the dissolution rate of zinc under atmospheric moisture and salt exposure.
Self-Healing Cut Edges
When ZM coated steel plates are sheared, punched, or scratched, $Mg^{2+}$ and $Al^{3+}$ ions dissolve and migrate across the un-coated steel edge. They form a compact, insoluble protective film dominated by Simonkolleite [$Zn_5(OH)_8Cl_2\cdot H_2O$] and basic magnesium carbonate, completely sealing the exposed steel core against red rust.
Tribological & Friction Superiority
The addition of Magnesium significantly increases surface hardness ($HV \ge 130-160$). This drastically reduces surface galling, flaking, and zinc powdering during aggressive roll-forming, deep drawing, and press stamping operations, keeping tooling clean and extending die service life.
In rigorous neutral salt spray testing ($NSS$), traditional Hot-Dipped Galvanized ($HDG$, $Z275$) exhibits red rust formation around 500 to 800 hours. Galvalume ($AZ150$) reaches 1,500 hours before edge breakdown occurs. By contrast, a **Zinc-Aluminum-Magnesium coating ($ZM275$) easily surpasses 4,500 to 6,000+ hours** without red rust propagation on flat surfaces or cross-hatched cut edges. This exceptional performance allows design engineers to replace post-hot-dip galvanizing process chains with direct pre-coated ZM sheet fabrication, cutting total component costs by 20% to 35%.
Global Sourcing Requirements & Sector Solutions
How Tier-1 contractors, solar tracker manufacturers, OEM automotive stampers, and agricultural engineers deploy Zn-Al-Mg coated steel plates to eliminate corrosion vulnerabilities.
Solar Photovoltaic (PV) Mounting Structures
Photovoltaic projects in desert environments (high abrasion), coastal salt flats (C5-M corrosion rating), and agricultural solar farms require a 25-to-30-year design life. Replacing heavy batch hot-dip galvanized steel profiles with high-strength **ZM275 / ZM310 / ZM430** roll-formed torque tubes, purlins, and ground posts eliminates batch galvanizing logistics, prevents deformation of thin-walled members, and ensures complete edge-protection along pre-punched mounting holes.
Automotive Chassis & EV Battery Enclosures
Automotive OEMs face demanding lightweighting and anti-corrosion standards for EV battery trays, suspension arms, subframes, and structural underbody components exposed to road salts and gravel impacts. Zn-Al-Mg coated plates ($DX53D+ZM$, $DX54D+ZM$) deliver superior drawability and weldability while maintaining anti-corrosion barrier integrity even after harsh stone-chipping and mechanical bending.
Agricultural & Livestock Housing Structures
Swine, poultry, and dairy farming environments accumulate severe concentrations of ammonia ($NH_3$), hydrogen sulfide ($H_2S$), high humidity, and organic acids. Conventional galvanized steel sheets undergo rapid white and red rust degradation within 3 to 5 years. Zn-Al-Mg steel forms an inert magnesium-hydroxide surface passivating layer that resists chemical alkali/acid exposure, extending building skin and frame life beyond 20 years.
Coastal Infrastructure & Highway Engineering
Highway sound barriers, guardrails, cable trays, air-conditioning outdoor condenser cabinets, and sea-wall structural framing require ultimate resistance to marine salt aerosol spray. ZM plates provide a maintenance-free substitute for stainless steel or post-painted assemblies, lowering lifetime infrastructure life-cycle expenditure ($LCC$).
Continuous Galvanizing Line (CGL) Process & Tech Roadmap
Our state-of-the-art continuous hot-dip zinc-aluminum-magnesium alloy line incorporates automated air-knife gauge stabilization, online infrared thermography, and eco-friendly chemical passivation.
Substrate Cleaning & Annealing
Cold-rolled or hot-rolled pickled coil is degreased in an electrolytic alkali bath and reduced in a vertical radiant-tube furnace under a $N_2 / H_2$ protective atmosphere to ensure pristine surface reactivity.
Molten Bath Chemistry Control
Substrate enters the molten pot maintained precisely at $430^\circ C - 470^\circ C$. Continuous electromagnetic stirring guarantees homogeneous distribution of $Zn-Al-Mg$ elements without chemical segregation.
Air-Knife Dynamic Wiping
High-pressure nitrogen or air knives wipe excess molten alloy to achieve closed-loop coating weight regulation ranging from $ZM90$ ($90g/m^2$) up to heavy-duty $ZM600$ ($600g/m^2$) with $\pm 3\%$ precision.
Cooling & Passivation
Controlled cooling rates refine the ternary eutectic grain boundaries. A chrome-free, RoHS/REACH compliant organic or inorganic passivation layer is sprayed to prevent storage wet-stain/white-rust.
Our engineering team is driving two key technical innovations: **1) Zero-Carbon Substrate Integration**, coupling hydrogen-reduced DRI iron with low-carbon melt-shops to provide net-zero embodied carbon ZM steel plates; **2) Ultra-High-Strength ZM Structural Steels ($S550GD+ZM, S700GD+ZM$)**, providing structural designers with high yield strength alongside maximum environmental durability for next-generation solar tracker torque beams and lightweight commercial vehicle chassis.
Comprehensive Engineering Specifications & Material Matrix
Full compliance with international standards including EN 10346, ASTM A1046 / A1046M, JIS G3323, and GB/T 34299. Custom dimensions cut-to-length or supplied as master coils.
| Coating Designation | Nominal Alloy Composition | Coating Mass Range (g/m²) | Equivalent Single-Side Thickness | Recommended Service Environment | Primary Suitable Steel Grades |
|---|---|---|---|---|---|
| ZM90 / ZM120 | Zn + 1.5% Al + 1.5% Mg | 90 - 120 g/m² | ~7 - 10 µm | Mild Rural / Indoor Appliances / HVAC | DX51D+ZM, DX52D+ZM, Commercial Quality |
| ZM180 / ZM220 | Zn + 2.0% Al + 2.0% Mg | 180 - 220 g/m² | ~14 - 17 µm | Industrial Roofs, Urban Framing, Cable Trays | DX53D+ZM, S280GD+ZM, S350GD+ZM |
| ZM275 / ZM310 | Zn + 3.0% Al + 3.0% Mg | 275 - 310 g/m² | ~20 - 24 µm | Solar PV Mounting, Agriculture, Guardrails (C4/C5) | S350GD+ZM, S420GD+ZM, S550GD+ZM |
| ZM430 / ZM600 | Zn + 6.0% Al + 3.0% Mg | 430 - 600 g/m² | ~32 - 45 µm | Extreme Coastal (C5-M), Subsea Ports, Heavy Chemical | S350GD+ZM, Heavy Structural Plate Substrates |
Thickness & Width Dimensional Capability
Thickness: 0.40 mm to 6.0 mm
Width: 600 mm to 1600 mm
Coil ID: 508 mm / 610 mm
Coil Weight: Up to 25 Metric Tons
Surface Finish Options
Spangle: Zero Spangle / Minimized Spangle
Passivation: Chrome-Free Passivation, Oiled, Anti-Fingerprint (AFP), Organic Sealer Coating
Secondary Processing
Precision Slitting, Cut-to-length Sheets, Punching, Roll-Forming Profiles, Stamping, Laser Cutting, Bending
Quality Assurance, Testing & Export Packaging
How we eliminate procurement risks for global buyers through rigid quality testing, mill test certificates (MTC), and ocean-going export protection.
Mill Test Certificate (MTC 3.1 / 3.2)
Every shipment is dispatched with an EN 10204 3.1 Mill Test Certificate detailing chemical ladle analysis ($C, Mn, P, S, Al, Mg$), mechanical yield/tensile testing, elongation ($A_{80}$), coating weight triple-spot test results, and bend test verification.
Third-Party Inspection Support
We welcome third-party international quality verification agencies including SGS, BV, Intertek, and Lloyd's Register for pre-shipment dimensional checks, coating thickness gauge audits, and salt spray coupon testing.
Seaworthy VCI Export Packaging
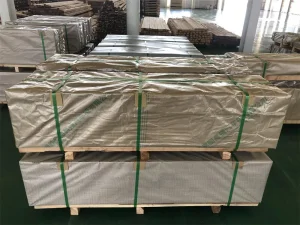
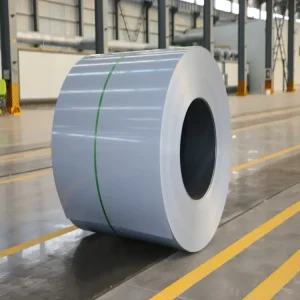
Coils and cut plates are wrapped with Volatile Corrosion Inhibitor ($VCI$) protective paper, sealed with heavy-duty galvanized steel inner/outer protective rings, wrapped in waterproof plastic film, and secured on fumigated wooden skids for containerized or break-bulk sea transport.
Frequently Asked Technical & Sourcing Questions
Detailed technical solutions for engineering teams, procurement directors, and plant metallurgists evaluating Zn-Al-Mg steel coil and plate adoption.
Silicon Steel, Galvannealed & Custom Pipe Offerings
Discover our comprehensive mill portfolio, covering electrical silicon steel coils, galvannealed sheets, tinplate, and structural hollow sections.