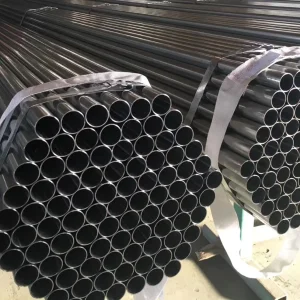
Mill-direct structural steel, high-frequency welded thin-wall tubing, coated coils, and special electrical steel solutions engineered for global industrial buyers.





A rigorous technical analysis of Electric Resistance Welded (ERW) and High-Frequency Induction Welded (HFIW) thin-wall steel tubing in modern industrial infrastructure.
The global demand for high-quality welding thin-wall steel tubing is undergoing a structural paradigm shift. Driven by automotive mass-reduction targets, rapid expansion of solar tracking arrays, modular building construction, and ergonomic structural furniture design, B2B buyers no longer evaluate suppliers solely on raw commodity pricing. Today’s industrial procurement ecosystem prioritizes strict dimensional tolerances, metallurgically sound weld seams, minimal ovality, superior surface cleanliness, and predictable yield-to-tensile ratios.
Precision thin-wall tubular products rely on cold-rolled steel coils (CR), pre-galvanized (GI) strips, or specialized alloy substrates (such as Zinc-Aluminum-Magnesium and Galvannealed ZF alloys). As a leading direct manufacturer and global wholesaler situated in Tianjin, China's premier steel hub, SMSTEEL integrates advanced continuous high-frequency induction welding (HFIW) lines capable of operating at fine-tuned mill speeds with real-time eddy current non-destructive testing (NDT).
Welding thin-wall carbon and alloy steel tubing introduces distinct metallurgical challenges compared to heavy-wall structural hollow sections. When the wall thickness drops below 1.5mm, thermal energy input during High-Frequency Induction Welding must be modulated with microsecond precision. Excess thermal energy causes burn-through, molten metal expulsion, and severe undercut; insufficient heat results in cold laps, lack of fusion, or micro-porosity along the longitudinal joint.
Our automated production facilities overcome this through state-of-the-art solid-state HFIW generators operating in the 300 kHz to 500 kHz frequency spectrum. This high-frequency skin effect concentrates electrical current along the extreme edges of the formed steel strip, heating only the immediate mating surfaces to forging temperature before squeeze rolls press them together, creating a solid-state forged weld free of cast structures and filler metals.
Examining regional demand drivers, supply chain resilience, and localized application scenarios across international B2B markets.
Global EV automakers and Tier-1 suppliers demand thin-wall ERW steel tubes (DP590, DP780, and DC04 grades) for seat frames, instrument panel beams, and chassis cross-members. High yield strength combined with controlled wall uniformity minimizes vehicle mass without sacrificing crash crashworthiness.
Modern commercial greenhouses and utility-scale solar farms require high-zinc (Z275 to Z600) pre-galvanized or hot-dip galvanized thin-wall circular and rectangular hollow sections. These tubes resist severe atmospheric corrosion while supporting structural loading across 25+ year operational lifespans.
Thin-wall steel conduits (EMT / IMC) and heat exchanger tubing require precise inside flash removal (ID scarfed) and uniform bendability. Suppliers must ensure zero micro-cracking during 90-degree rotary draw bending and cold flaring procedures.
For international stockists and OEM purchasing managers, buying thin-wall steel tubing at wholesale volumes introduces specific supply chain vulnerabilities, including transit corrosion (white rust), transport bundle deformation, and batch-to-batch chemical variance. SMSTEEL addresses these risks through a robust 5-point quality assurance framework:
- Raw Material Traceability: Sourcing high-grade hot-rolled pickled & oiled (HRPO) and cold-rolled (CR) strip coils exclusively from top-tier primary steel mills with full Mill Test Certificates (MTC to EN 10204 3.1).
- Continuous ID & OD Flash Scarfing: Automated carbide tooling planes down internal weld beads to an ultra-flat height (≤ 0.1mm), preventing obstruction in fluid lines or electrical cable pulling.
- Automated Seam Re-Galvanizing: For pre-galvanized tubing, an online thermal zinc wire spraying system immediately covers the scraped weld seam with a protective zinc layer equal in weight to the parent metal strip.
- Seaworthy Heavy-Duty Packaging: Hexagonal bundle strapping with plastic edge protectors, waterproof VCI anti-corrosion film wrapping, and timber dunnage blocks for containerized or break-bulk shipping.
- Flexible Trial Order Protocols: Accepting smaller initial sample shipments to allow purchasing clients to test ductility, flareability, and coating adhesion prior to executing large annual supply agreements.
Inside the continuous roll-forming, high-frequency welding, online heat treatment, and surface finishing lines at SMSTEEL's Tianjin facility.
Producing thin-wall steel tubing that satisfies stringent international standards (ASTM A513, EN 10305-3, JIS G3445) demands complete control over every stage of the mechanical roll-forming and thermal welding cycle. Below is the technical roadmap followed across our 8 automated production lines:
Master coils are precision slit on CNC gang slitters to width tolerances of ±0.05mm. Edge condition is continuously monitored to prevent burrs that could disrupt induction current distribution during welding.
Slit strip enters a multi-stand breakdown and fin-pass roll cluster. Specialized CAD/CAM designed roll profiles gradually form the flat strip into a open circular profile without inducing localized work-hardening.
Induction coils energize the strip edges. Squeeze rolls force the superheated edges together. Online pyrometers continuously adjust generator power based on line speed, maintaining an ideal forging temperature window (~1350°C).
Precision carbide inserts scrape the exterior squeeze-out and interior weld flash while molten. Immediate inline seam re-galvanizing applies zinc atomization over pre-galvanized weld zones.
The tube passes through sizing stands to achieve exact outer diameter, roundness, or shape conversion (into Square SHS or Rectangular RHS profiles) while strictly controlling corner radii and wall thickness integrity.
100% inline Eddy Current testing detects longitudinal micro-fissures or weld gaps. High-speed cold flying saws cut the tubing to precise customer lengths without burrs or thermal distortion.
As industrial automation advances, SMSTEEL is deploying AI-driven vision systems and closed-loop thermal imaging to monitor weld pool dynamics in real time. Future developments include laser-hybrid induction welding for ultra-thin stainless steel and high-strength low-alloy (HSLA) tubes, lowering energy consumption by up to 25% while producing a heat-affected zone 50% narrower than conventional ERW lines.
Tailored steel engineering packages developed for specific sector challenges, compliance mandates, and performance benchmarks.
Challenge: Standard steel tubing often suffers from visible weld seams, uneven powder-coating adhesion, and surface telegraphing after bending.
SMSTEEL Engineering Package: We supply Cold-Rolled Pickled ERW thin-wall tubing (0.7mm - 1.2mm wall thickness) featuring ultra-smooth matte surface finishes (Ra < 0.4 µm) and fully flattened internal weld seams. Ideal for chrome plating, electrostatic powder coating, and tight-radius rotary bending without wrinkling.
Challenge: High ambient humidity, fertilizer exposure, and wind loading require high strength combined with aggressive corrosion resistance.
SMSTEEL Engineering Package: Pre-galvanized and Hot-Dip Galvanized circular/oval tubes featuring high zinc coating density (up to Z450 / 450g/m²). Seams are sealed with secondary zinc thermal arc spraying, ensuring zero red rust formation under salt-spray testing for over 1,500 hours (ASTM B117 standard).
Challenge: Electrical equipment manufacturers require matching tubing and magnetic silicon steel raw materials with minimal core loss.
SMSTEEL Supply Chain Package: Integrated shipments combining pre-galvanized thin-wall conduit tubing alongside cold-rolled non-grain-oriented (CRNGO) silicon steel coils (M310–M800 grades), streamlining procurement and reducing freight costs for electrical OEM manufacturers.
Comprehensive engineering parameter matrix for thin-wall welded steel tubing, galvanized coils, and specialty steel substrates.
| Category / Specification | Common Standard | Grade / Alloy | Wall Thickness / Gauge Range | Outer Diameter / Dimension | Key Performance Attribute |
|---|---|---|---|---|---|
| ERW Thin-Wall Round Tube | ASTM A513 / EN 10305-3 | 1008 / 1010 / E195 / E235 | 0.5 mm – 2.0 mm | 9.5 mm – 76.2 mm | Ultra-smooth finish, tight OD tolerance (±0.05mm), excellent flareability. |
| Pre-Galvanized Square (SHS) | ASTM A500 / EN 10219 | Q195 / Q235 / S235JRH | 0.6 mm – 2.5 mm | 12×12 mm – 80×80 mm | Uniform zinc layer (60-200g/m²), continuous seam re-galvanized, clean corners. |
| Pre-Galvanized Rectangular (RHS) | GB/T 3091 / BS EN 10219 | Q235B / S275J0H | 0.7 mm – 2.5 mm | 10×20 mm – 40×100 mm | High torsional resistance, ideal for light structural frames and solar purlins. |
| Hot-Dip Galvanized Pipeline | ASTM A53 / BS 1387 / EN 10255 | Grade A, B / S235GT | 1.2 mm – 3.5 mm | 1/2” – 4” NB (21.3 - 114.3mm) | Heavy zinc coating (≥ 300g/m² inside & out), hydrostatic pressure tested to 5MPa. |
| Cold-Rolled Pickled Coil (HRPO) | ASTM A1011 / JIS G3131 | SPHC / SPHD / DD11 | 1.5 mm – 4.0 mm | Coil Width 600 - 1500 mm | Scale-free pickled surface, optimized for tube roll-forming and deep drawing. |
| Galvannealed Steel Coil (ZF) | ASTM A653 / EN 10346 | ZF60 – ZF275 / DX51D+ZF | 0.4 mm – 2.0 mm | Coil Width 800 - 1250 mm | Zinc-Iron alloy layer, superior spot welding capability and immediate paintability. |
| Silicon Steel Coil (CRNGO) | IEC 60404-8 / GB/T 2521 | M310 / M350 / M470 / M800 | 0.35 mm – 0.50 mm | Coil Width 900 - 1200 mm | Low core loss, high magnetic permeability for high-efficiency electric motor rotors. |
Addressing critical procurement, metallurgical, and manufacturing questions from engineering buyers and global importers.
Explore our full line of hollow sections, electrical silicon steels, pre-galvanized structural tubes, and hot-dip galvanized agricultural piping.