
Featured Cold-Rolled & Coated Steel Products
Explore our export-grade flat steel coils, specialty thin plates, and processed strip lines manufactured under strict ISO 9001 quality controls.
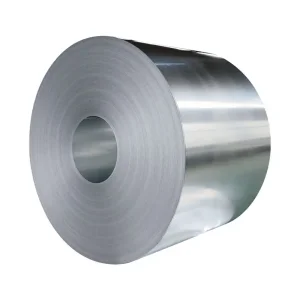






Technical Whitepaper: Cold-Rolled Thin Steel Plate Engineering
An authoritative analysis of mechanical deformation, recrystallization annealing, thickness control algorithms, and surface topography optimization in modern cold reduction mills.
Cold-rolled thin steel plates represent the pinnacle of precision flat-rolled metalworking. Unlike hot-rolled counterparts processed above recrystallization temperatures, cold-rolled sheets undergo room-temperature mechanical reduction. This cold work hardening process imparts exceptional yield strength, ultra-smooth surface textures, precise dimensional tolerances, and superior drawability required for high-stakes manufacturing across automotive, aerospace, precision electronics, and industrial appliance sectors.
1. Process Metallurgy: From Hot-Rolled Substrate to Cold-Reduced Sheet
The manufacturing journey begins with high-grade hot-rolled pickling coils (SPHC/Q235/S235JR base stock). Hydrochloric acid pickling removes the iron oxide scale ($Fe_2O_3, Fe_3O_4, FeO$) formed during hot rolling. The descaled strip enters a continuous 4-high or 6-high tandem cold rolling mill or a reversible Sendzimir 20-high cluster mill.
During cold reduction, grains are elongated along the rolling direction, generating high dislocation density and severe lattice distortion. This work hardening elevates hardness (often reaching HRB 85–95 in full-hard state SPCC-1B) while reducing ductility. To restore formability for deep-drawing applications, the hard-rolled coils undergo recrystallization annealing:
- Continuous Annealing Line (CAL): The strip passes through heating, soaking, and rapid cooling zones in a protective atmosphere ($H_2-N_2$ gas mix) within minutes. CAL yields highly consistent mechanical properties, superior flatness, and controlled grain size distribution.
- Batch Annealing / Bell Furnace (BA): Coils are stacked inside sealed protective inner covers and heated over long thermal cycles (30–50 hours). Batch annealing provides deep stress relief and exceptional ductility, optimal for deep drawing grades like SPCD, SPCE, and DC04/DC06.
2. International Standard Cross-Reference Matrix
Global procurement teams must navigate diverse national and international standards. Below is a comprehensive engineering cross-reference for cold-rolled mild steel plates and coils:
| Commercial / Quality Standard | JIS G3141 (Japan) | EN 10130 / 10139 (Europe) | ASTM A1008 / A1008M (USA) | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation $A_{50}$ (%) |
|---|---|---|---|---|---|---|
| Commercial Quality | SPCC | DC01 | CS Type A / B / C | 140 – 280 | 270 – 410 | ≥ 28 |
| Drawing Quality | SPCD | DC03 | DS Type A / B | 140 – 240 | 270 – 370 | ≥ 34 |
| Deep Drawing Quality | SPCE | DC04 | DDS (Deep Drawing) | 140 – 210 | 270 – 350 | ≥ 38 |
| Extra Deep Drawing (IF Steel) | SPCF / SPCG | DC05 / DC06 | EDDS (Extra Deep Draw) | 110 – 180 | 270 – 330 | ≥ 42 |
| High Strength (Structural) | SPFC 340-590 | HC260LA / HC340LA | HSLAS Grade 45-80 | 260 – 550 | 340 – 650 | ≥ 18 |
Manufacturing Capacity & Quality Assurance Benchmarks
Why Sourcing Cold-Rolled Thin Plates from China Delivers Superior Value
Strategic industrial integration, ultra-modern rolling mill equipment, and uncompromised supply chain efficiency in Tianjin and Bohai Bay steel hub.
Integrated Supply Chain Synergy
Our facility sits directly within China’s premier Bohai Rim steel manufacturing cluster. Direct liquid iron sourcing from upstream mega-blast furnaces and immediate access to top-tier pickling lines eliminate intermediate transport costs and thermal energy loss, passing maximum cost benefits to global buyers.
Next-Gen Mill Automation & QC
Equipped with state-of-the-art 6-high reversible cold rolling mills, automated shape meters (VC roll tech), and real-time surface defect detection sensors, our factory maintains precise crown and strip flatness (within 5 IU - I-Units), minimizing scrap rates during downstream high-speed blanking.
Custom Metallurgy & Surface Finishing
Whether your application requires bright finish (Ra ≤ 0.2 µm) for electroplating, stone finish (Ra 0.2–0.6 µm), or dull/matte finish (Ra 0.6–1.2 µm) for excellent paint adhesion, our skin-pass (temper rolling) mills customize surface roughness to exact client parameters.
Global Industry Trends Shaping Thin Steel Plate Manufacturing
How decarbonization, electric vehicle light-weighting, and AI-driven rolling automation are revolutionizing flat steel technology.
1. Ultra-Thin Gauge Precision Rolling
As consumer electronics, lithium battery casings, and motor enclosures downsize, demand for thin-gauge steel plate under 0.20 mm is surging. Reversible 20-high cluster mills now produce ultra-thin cold-rolled plates with micron-level gauge consistency, replacing thicker traditional metals without sacrificing structural rigidity.
2. Advanced High-Strength Steels (AHSS)
The automotive transition toward Electric Vehicles (EVs) requires crash-resistant yet lightweight sheet metal. Modern cold rolling lines process Dual-Phase (DP590/780/980) and Complex-Phase (CP) steels, enabling auto-stamping plants to reduce vehicle body-in-white weight while boosting safety margins.
3. Decarbonization & Green Steel Initiatives
Global OEMs mandate low-carbon supply chains. Leading Chinese manufacturers are integrating Direct Reduced Iron (DRI) fed by green hydrogen, combined with EAF (Electric Arc Furnace) melting, drastically cutting $CO_2$ emissions per ton of cold-rolled finished coil to meet EU CBAM and global ESG frameworks.
Target Application Scenarios & Engineering Solutions
Tailored steel grades and custom slitting, oiling, and annealing recipes optimized for specific downstream processing environments.
Automotive Stamping & Panels
Recommended Grades: SPCD, SPCE, DC04, DC06, DP600
Key Requirements: Exceptional $r$-value (plastic strain ratio) and $n$-value (strain hardening exponent) to prevent wrinkle and tear formation during multi-stage progressive die stamping of vehicle doors, hoods, and structural brackets.
Home Appliances & Enclosures
Recommended Grades: SPCC-SD, DC01-A, ASTM A1008 CS
Key Requirements: Ultra-flat dull finish (Ra 0.8–1.2 µm) providing optimal mechanical keying for electrostatic powder coating, painting, and enameling on refrigerator side panels, washing machine drums, and HVAC chassis.
Precision Electrical & Transformer Core Base
Recommended Grades: Non-Oriented Silicon Steel Base / CRNGO Substrates
Key Requirements: Controlled magnetic permeability, low core loss ($W/kg$), tight gauge uniformity, and burr-free longitudinal slitting for motor laminations, distribution transformers, and ballast stampings.
Food Packaging & Canmaking (ETP/TFS Base Plate)
Recommended Grades: Single Reduced (SR) & Double Reduced (DR) CA Base
Key Requirements: Ultra-thin gauges (0.14–0.24 mm), precise temper hardness (T2 to T5, DR8 to DR9), and clean surfaces suitable for electrolytic tin plating or chrome coating used in aerosol cans and food containers.
Solar Mounting & Construction Framing
Recommended Grades: High-Zinc Coated (Z275/ZM275) / Galvannealed Base
Key Requirements: Superior yield strength combined with thick protective coatings (Zinc-Aluminum-Magnesium or Hot-Dip Galvanized) providing 25+ year corrosion resistance in harsh outdoor atmospheric conditions.
Steel Furniture & Office Storage
Recommended Grades: SPCC-1B (Full Hard) or Soft SPCC Annealed
Key Requirements: Sharp edge folding capability without surface micro-cracking, clean light oiling (1.0–2.0 $g/m^2$) for rust prevention during ocean transit, and high surface cleanliness.
Global Purchasing Standard Operating Procedures & QC Verification
How enterprise buyers mitigate cross-border quality risks through rigorous mill test reporting, non-destructive testing, and seaworthy packaging.
1. Quality Management Systems & Certifications
Enterprise procurement teams cannot rely solely on price. Reliable cold-rolled thin steel manufacturers operate under strict international quality management standards:
- IATF 16949: Essential certification for tier-1 automotive sheet suppliers, guaranteeing continuous process improvement, defect prevention, and reduction of variation and waste in the supply chain.
- ISO 9001 & ISO 14001: Core quality management and environmental safety benchmarks ensuring repeatable chemistry, mechanical properties, and sustainable emissions control.
- EN 10204 3.1 Mill Test Certificates (MTC): Full traceability provided with every shipment, detailing heat chemical composition (C, Mn, P, S, Si, Al, Ti), yield strength ($R_e$), tensile strength ($R_m$), elongation ($A_{50}$), hardness (HRB/HV), and average surface roughness ($R_a$).
2. Packaging & Seaworthy Logistics Specifications
Cold-rolled thin steel is highly susceptible to atmospheric oxidation (white/red rust) and edge damage during transoceanic shipping. Enterprise orders must enforce standardized export packaging:
VCI Anti-Rust Protection
Every coil/sheet bundle is completely wrapped in Volatile Corrosion Inhibitor (VCI) paper or film. VCI molecules evaporate and form an invisible protective monomolecular layer on the steel surface, inhibiting oxidation even in high-humidity maritime container trips.
Heavy-Duty Steel Wrapper
Outer galvanised steel jackets, corner protectors (inner and outer radial edge rings), and high-tensile steel strapping (minimum 4 circumferential and 3 radial straps) shield coils against mechanical impact during crane handling and port staging.
Vertical vs. Horizontal Palletization
Offered in both Eye to Sky (vertical axis, optimal for automatic uncoiler loading) and Eye to Wall (horizontal axis on wooden skids with fumigation ISPM 15 compliance), tailored to buyer port unloaders and factory cranes.
Complete Processing & Specialized Metal Lines
Explore our extended lineup of specialized coated products, tinplate, high-strength cold rolled sheet, and electrical steel solutions.






Technical & Sourcing Frequently Asked Questions
In-depth engineering answers addressing gauge tolerances, surface oils, mechanical testing, and cross-border logistics.
What is the difference between SPCC, SPCD, and SPCE cold-rolled steel grades?
Under the Japanese Industrial Standard (JIS G3141), SPCC denotes Commercial Quality steel intended for basic bending, forming, and light drawing. SPCD represents Drawing Quality steel with higher ductility and lower yield strength, suitable for deeper press work. SPCE is Deep Drawing Quality steel utilizing interstitial-free (IF) aluminum-killed metallurgy, formulated to prevent strain aging and stretcher strain marks during complex automotive body pressing.
What thickness tolerances and width limits can your cold rolling mill maintain?
Our 6-high reversible and tandem cold rolling mills maintain gauge tolerances within ±0.005 mm for thin sheets (0.12–0.50 mm) and within ±0.01 mm for standard gauges (0.50–3.00 mm). Available width ranges from 600 mm up to 1500 mm, with custom precision slitting available down to narrow strips of 15 mm with minimal burr height (< 0.02 mm).
Which surface finishes (roughness Ra) and oiling options are available?
We supply three main surface textures via skin-pass rolling: Bright Finish (B) ($R_a \le 0.2\,\mu\text{m}$) for high-reflection electroplating; Semi-Dull / Stone Finish (S) ($R_a = 0.2\text{--}0.6\,\mu\text{m}$); and Dull / Matte Finish (D) ($R_a = 0.6\text{--}1.2\,\mu\text{m}$) ideal for paint retention. Corrosion protective oil options include Light Oiling ($0.5\text{--}1.0\,\text{g/m}^2$), Standard Oiling ($1.0\text{--}2.5\,\text{g/m}^2$), Heavy Oiling, or Dry (DOS coated / chromated / passivated).
How do you prevent rust formation during long sea freight voyages?
All coils and sheet packs undergo a multi-layer protective protocol: inner electrostatic anti-rust oiling, hermetic wrapping with Volatile Corrosion Inhibitor (VCI) anti-rust paper, polyethylene plastic film sealing, galvanised steel outer armor wrap, steel corner protectors, and heavy-duty steel strapping anchored to fumigated wooden pallets or steel skids.
What testing documentation is included with EN 10204 3.1 Mill Test Certificates?
Every certificate provides full heat traceability. Certified data includes spectral ladle chemical analysis (C, Mn, P, S, Si, Al, N, Cr, Ni, Cu), mechanical tensile test results (Yield $R_e$, Ultimate Tensile $R_m$, Total Elongation $A_{50}$), Hardness (HRB/HV), Bend test compliance, $r$-value and $n$-value metrics for deep drawing, and average surface roughness $R_a$.
Can your factory produce high-strength automotive structural steels like DP590 or HC260LA?
Yes. Our continuous annealing and quenching line processes Dual-Phase steels (DP590, DP780) and High-Strength Low-Alloy (HSLA) grades like HC260LA and HC340LA under computer-controlled cooling profiles, combining high tensile strength with sufficient cold formability for vehicle chassis and safety cage components.
What is your standard Minimum Order Quantity (MOQ) and production lead time?
Standard production MOQ is 25 Metric Tons per thickness/width dimension (equivalent to one full 20ft container load). For standard grades (SPCC/DC01/DX51D) in stock master coil format, custom slitting and cut-to-length orders can be dispatched within 7 to 10 days. Custom mill rolling campaigns typically require 20 to 30 days.